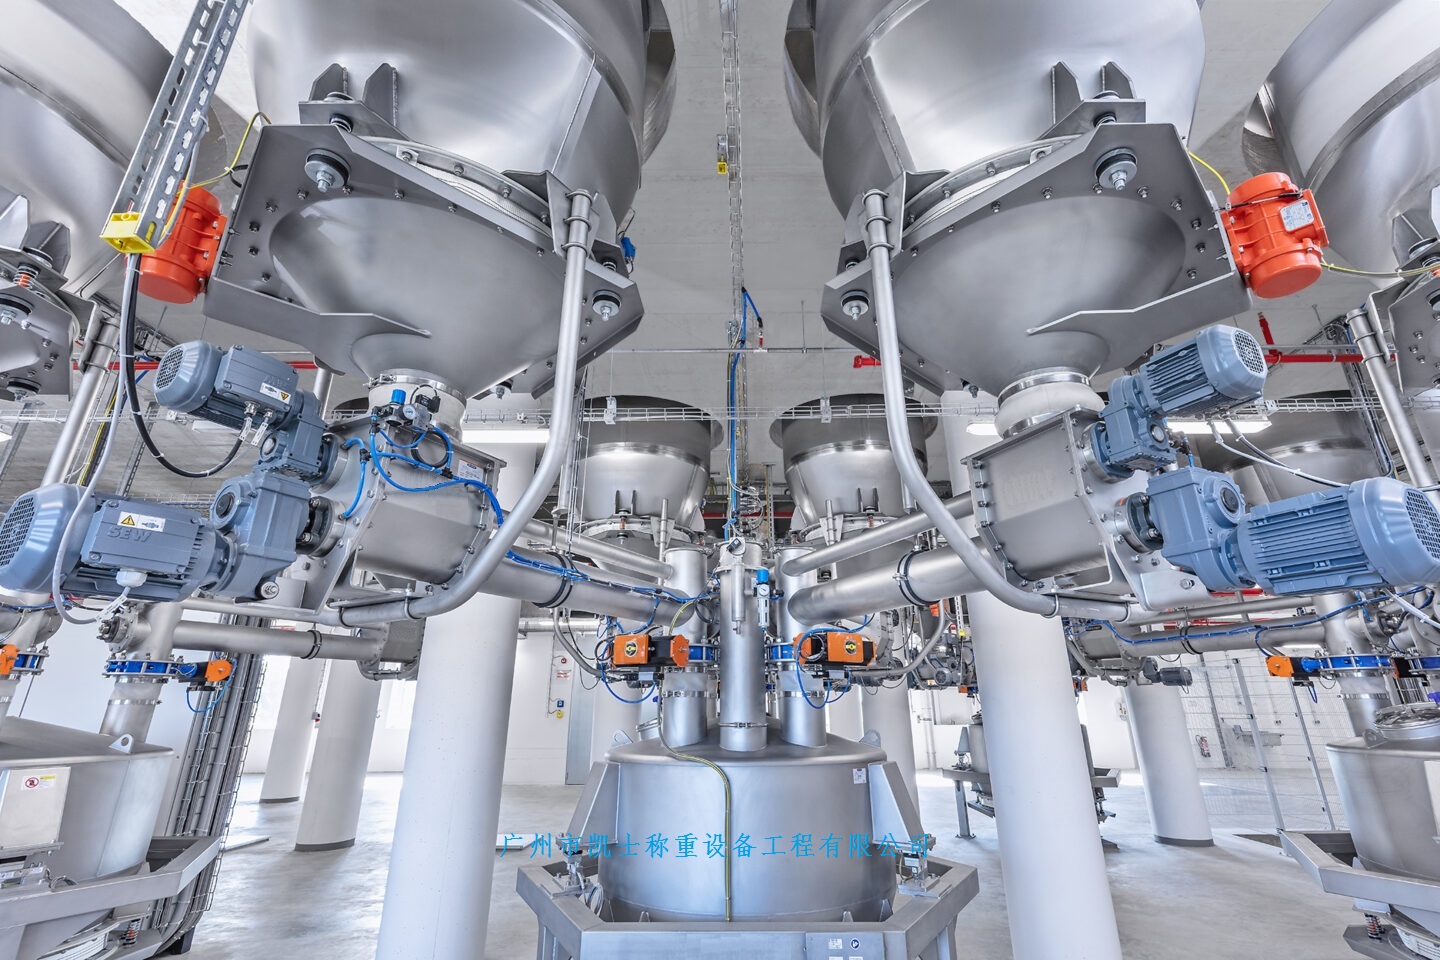
The hopper feeder achieves fast and slow feeding by controlling the input signal size of the frequency converter. Firstly, it performs fast feeding. Once the feeding reaches a certain value, the feeding speed gradually slows down. The stopping time of the feeding motor is adjusted by adjusting the starting torque of the frequency converter. By using multiple frequency converters to control multiple motors, the starting torque of each frequency converter can be adjusted separately to adjust the stopping time of each motor, thereby improving the weighing accuracy of various materials.

 020-34563445
The feeding system of the hopper scale is composed of a weighing sensor, a hopper scale, a screw Feeder and a PLC to form the Batching system. It is used to complete weighing, measurement, with PLC as the core, equipped with various electric actuators and mechanical devices, adopting a two-level feeding method. The coarse feeding flow is large, and within a short time, 90% to 95% of the rated weight can be added. The fine feeding flow is small, accounting for 5% to 10% of the rated weight. This realizes the dynamic online weighing and measurement of the materials. Above the hopper scale is the finished product storage area. The raw materials in this storage area are the granular finished products produced in the material mixing process. Below the finished product storage area is a motor-driven screw feeding device. When the motor is started, the powdered materials in this finished product storage area will rotate with the transmission cage and enter the hopper scale for weighing. Three strain-type Weighing modules are installed on the hopper scale. The mass signal of the hopper scale is directly converted by this weighing sensor group into a corresponding voltage signal. After the voltage signal is amplified by the hopper scale and sent to the PLC analog module for data processing, when it reaches the preset value, the PLC controls to stop feeding, then the PLC controls to open the hopper scale door and control the mixer to automatically batch. The automatic process of material weighing and batching is completed.
The materials are respectively placed in multiple storage bins. These multiple storage bins are arranged in a circle above the conical central funnel. The materials are successively fed into the hopper scale through the central funnel for weighing. The storage bins are divided into upper storage bins and lower storage bins. Various materials are placed in the multiple upper storage bins. The lower opening of the lower storage bin is connected to a screw feeder to prevent the screw feeder from being "blocked" by the materials. Positioning sensors of the upper and lower moving types are set in the lower storage bin to prevent the screw feeder from being blocked. When the materials reach the lower loading position of the lower storage bin, the valve of the lower storage bin is closed. When the weight of the materials in the lower storage bin reaches the set value, the PLC outputs a signal to quickly close the bin door of the hopper scale, then opens the discharge bin door of the hopper scale, and the materials fall into the mixing machine at the loading position. Thus, the weighing task is completed. Subsequently, the mixing system completes automatic batching, guides the finished product materials falling from the chute to the next process, and the scraper is used to prevent the finished product materials from sliding. When opening the bin door of the hopper scale, sometimes due to reasons such as blockage of the bin door, the materials may not be completely dropped into the mixing machine by the hopper scale. Therefore, three weighing sensors (corresponding to the batching weight) are set to detect whether the materials have completely entered the mixing machine.
The hopper scale achieves fast and slow feeding by controlling the input signal size of the frequency converter. Firstly, it performs fast feeding. When the feeding reaches a certain value, the feeding speed gradually slows down. The stopping time of the feeding motor is adjusted by adjusting the starting torque of the frequency converter. Using multiple variable frequency converters to control multiple motors allows for adjusting the starting torque of each frequency converter to adjust the stopping time of each motor, thereby improving the weighing accuracy of various materials. The control system first starts the 1# screw feeder, continuously feeding materials to the hopper scale at full speed. The hopper scale conducts continuous weighing. When a certain value of the weighing value is reached, the speed of the screw feeder begins to decrease (through frequency conversion speed regulation), and as the amount of materials increases, the speed of the screw feeder becomes slower. When the weighing value approaches or reaches the required value, the screw feeder stops. At this point, the weighing of the first type of material is completed. Open the discharge valve of the hopper scale to place the materials in the intermediate storage bin for temporary storage. Then start the 2# feeder to weigh the second type of material. After each type of material is weighed and placed in the intermediate storage bin for temporary storage, all the materials are weighed together and then placed in the porcelain mill for mixing with water and sent to the next process.