


















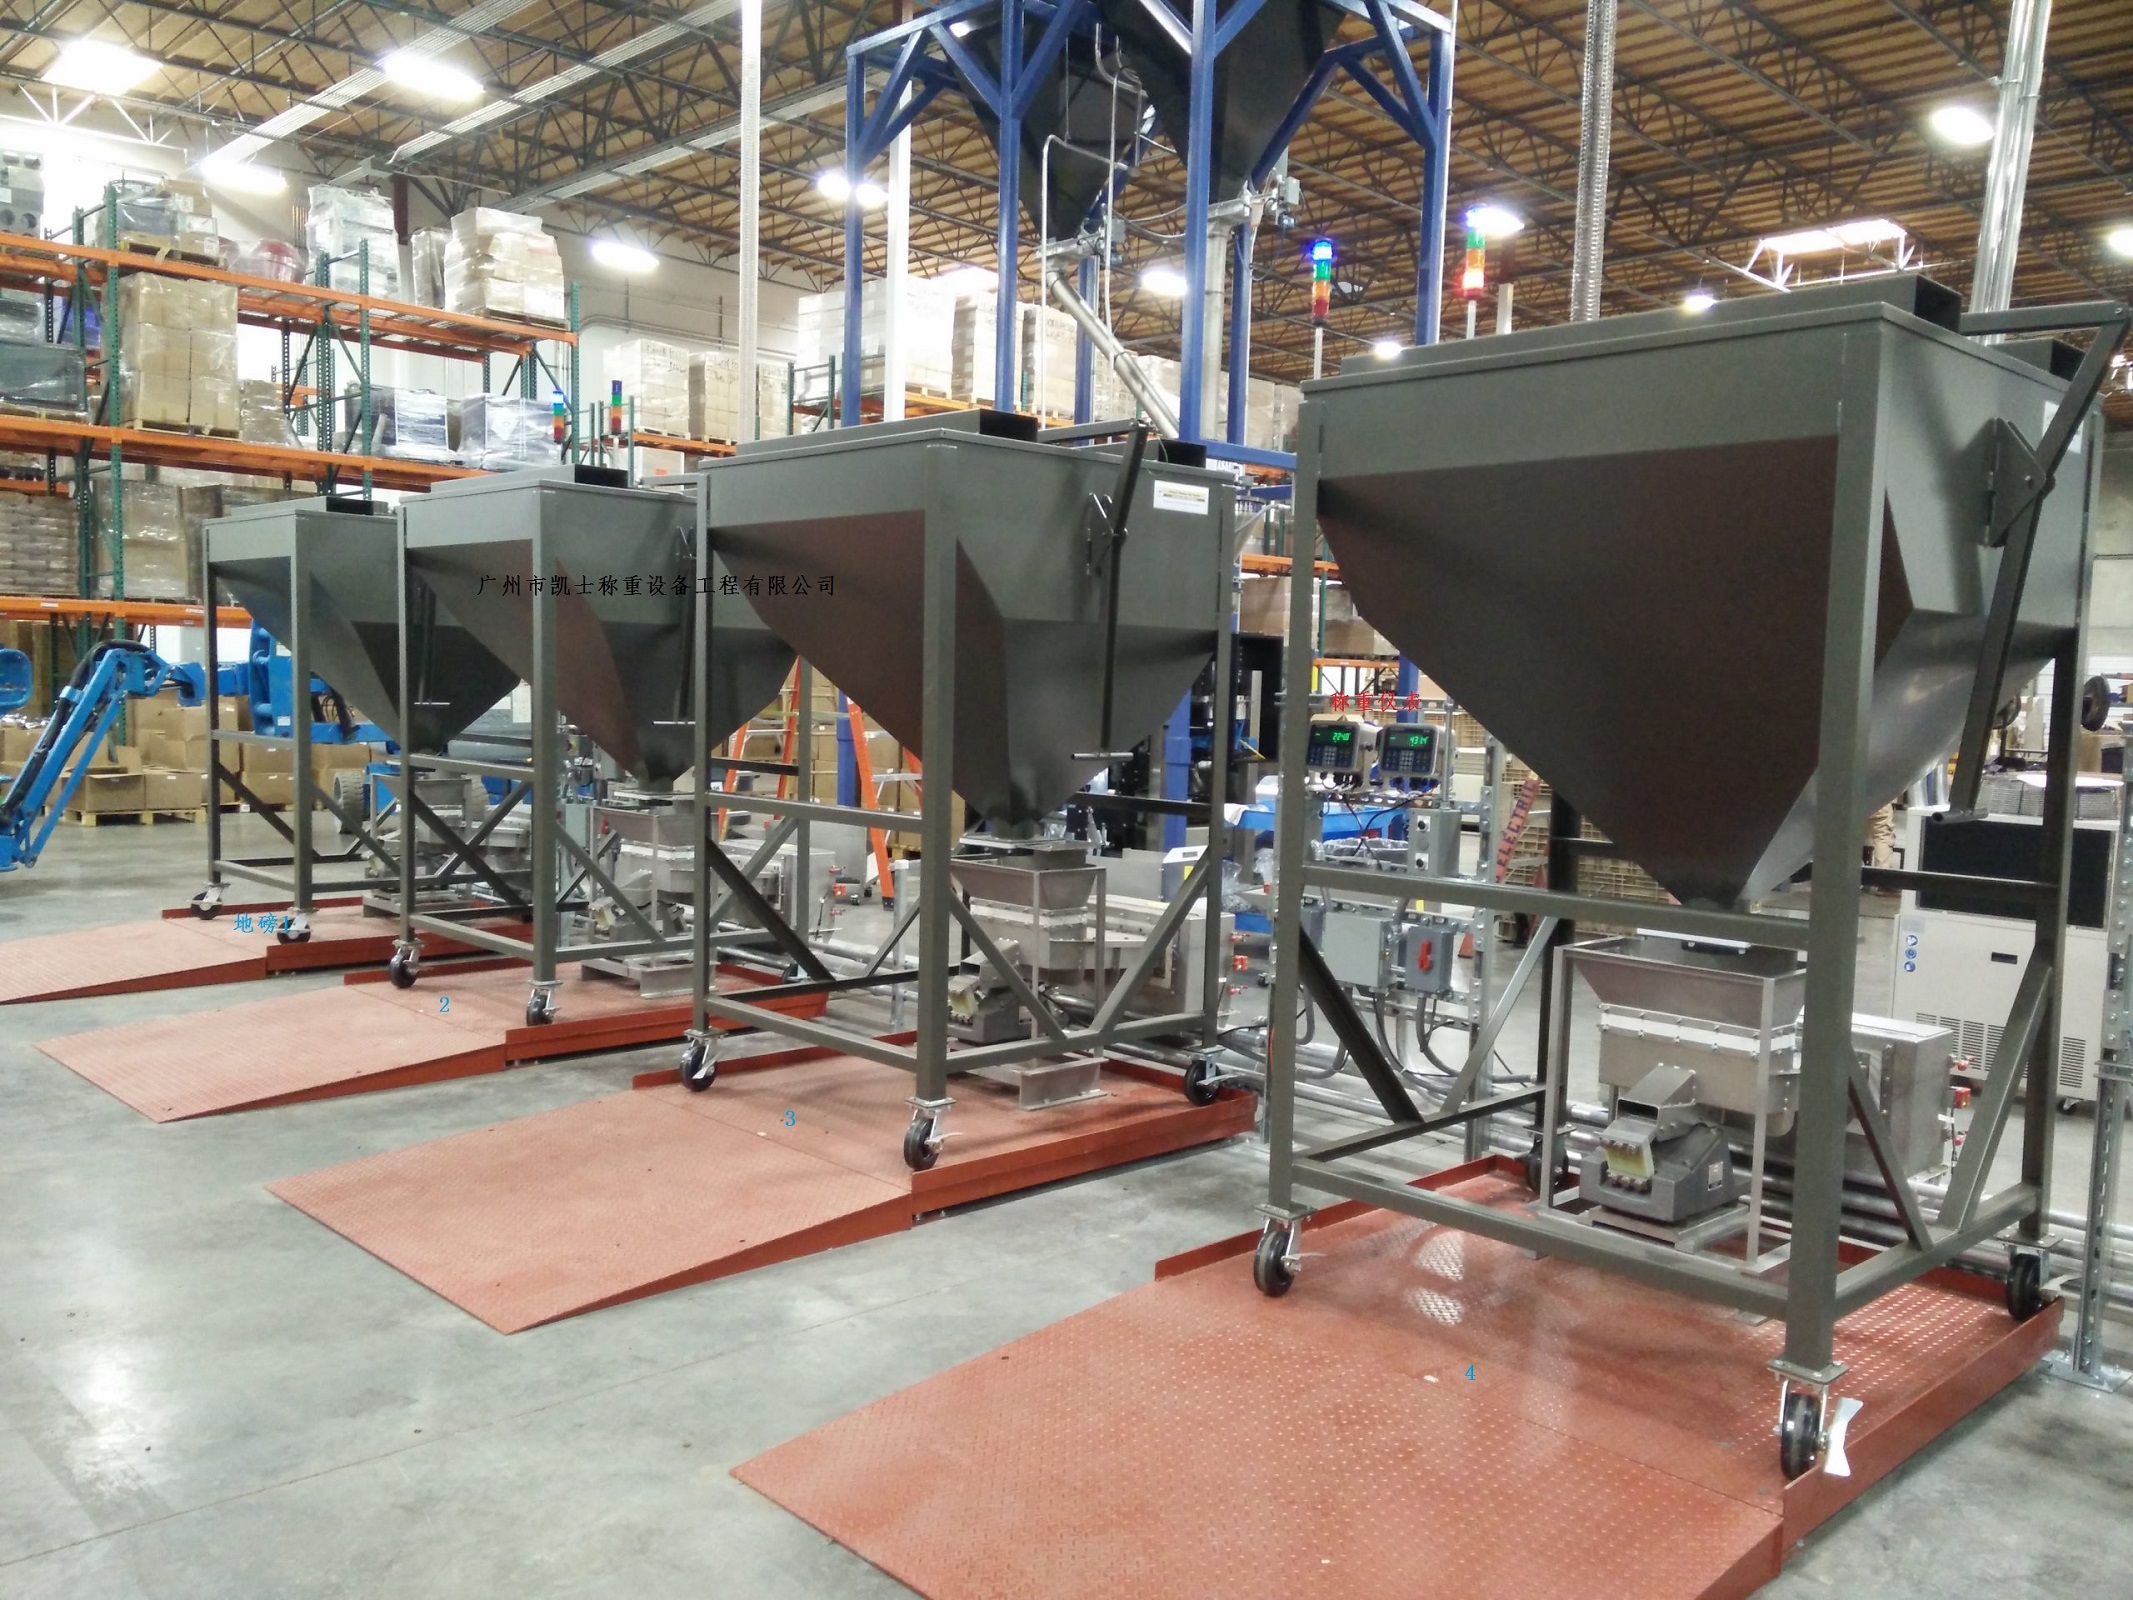
Self-control Electronic floor scale is a weighing equipment integrating automatic weight measurement, dosing and alarm. It is an automatic weighing system, which consists of weighing platform, electrical control system, pneumatic valve and so on. It is characterized by the following features: LED display on the silo and weighing circuit board next to the LED display, which realizes the functions of automatic data collection, automatic recording and printing, and one-key test. Through the automatic data collection and uploading server system, it provides valuable basic data for the big data research currently being carried out.



 020-34563445
The self-controlled scale integrates automatic weighing, batching, and alarm functions. It is a type of automatic Weighing system consisting of a scale platform, an electrical control system, and pneumatic valves, etc. An LED display is installed on the silo, and a weighing instrument is placed beside the LED display, enabling automatic data collection, automatic recording, printing, and other functions, and achieving one-click testing. Through the automatic collection and upload of data to the server system, it provides valuable basic data for the current big data research. The Electronic scale mainly consists of a touch screen + PLC (industrial computer control system) and automatic pneumatic valves, conveying pumps, mixing tanks, and weighing systems, etc. The electronic scale can automatically mix and proportion various raw and auxiliary materials in different sequences and at different temperatures through the automatic control program of the PLC touch screen, achieving the ideal automated batching and weighing equipment for product production.
A centralized control operation console is set up at the ingredient production site. The dynamic weighing and metering instruments are installed on the console. The electronic floor scale installed at the lower part of the support legs of the metering tank is connected to the dynamic metering instrument. The real-time data is transmitted from the metering instrument through the communication line to the industrial control computer in the control center. The formula and control commands are sent from the industrial control computer in the control center to the instruments and PLC controllers via the communication line. An air-operated control valve is installed at the feed inlet of the metering silo to achieve rapid and slow feeding control of the materials. The materials can be directly added into the metering silo through the screw Feeder, and the weight of the materials entering the metering silo will automatically stop when it reaches the designated weight valve. After the material measurement is completed, it is automatically added to the corresponding mixing silo through the automatic分流device at the bottom of the metering silo.
The ingredient scale is equipped with a scale, a control system and several spiral silos. On the spiral silos, there are pneumatic regulating valves for controlling the water volume. The electronic scale, each pneumatic regulating valve and the control system are electrically connected. The control system is equipped with a weight setting module for setting the weight of the material released from each spiral silo, and a time setting module for setting the opening interval time of each pneumatic regulating valve. By setting the pneumatic regulating valves and the scale, and controlling the closing and opening size of the valves through the control system, when the scale shows a weight close to the set weight value, the opening of the pneumatic regulating valve becomes smaller, and the material flows out at a low flow rate, ensuring the accuracy of weighing. Moreover, by setting the opening interval time of each pneumatic regulating valve through the time setting module, it can meet the requirements of sequential weighing, individual weighing and mixed weighing of various materials.
The ingredient weigher connects various materials through a screw conveyor from the hopper to the silo. There are pneumatic gates between the conveyor and the silo, which can control the material to be fed to the designated silo. An interlock alarm system composed of a rotary sensor is installed on the silo top. At the bottom of each silo, there is a screw conveyor. During the ingredient preparation, the program control is carried out by PLC according to the preset formula, and each screw conveyor is successively pushed to the weigher hopper for weighing. The weighing procedure is one material at a time. The sequentially entered materials are mixed and stirred. After the mixing is complete, the mixer starts to discharge the materials to the finished product silo until the discharge is finished, then the weighing and preparation for the next batch are carried out. At the top of the finished product silo, there is also a rotary sensor. When the finished product silo is full, the weighing and preparation for ingredients stops. When the material level is below the upper limit position, the process resumes and continues to weigh the materials. The entire system can be divided into two parts: the weighing and ingredient preparation process before the silos, and the weighing and ingredient preparation process after the silos. The task of the ingredient preparation process is to transport each material in the product ratio from the conveyor and screw conveyor to the designated silos as a preparation for the ingredient weighing control. The task of the ingredient preparation process is to weigh the materials in each silo, and send them into the screw mixer in proportion according to the formula to mix into the product.


