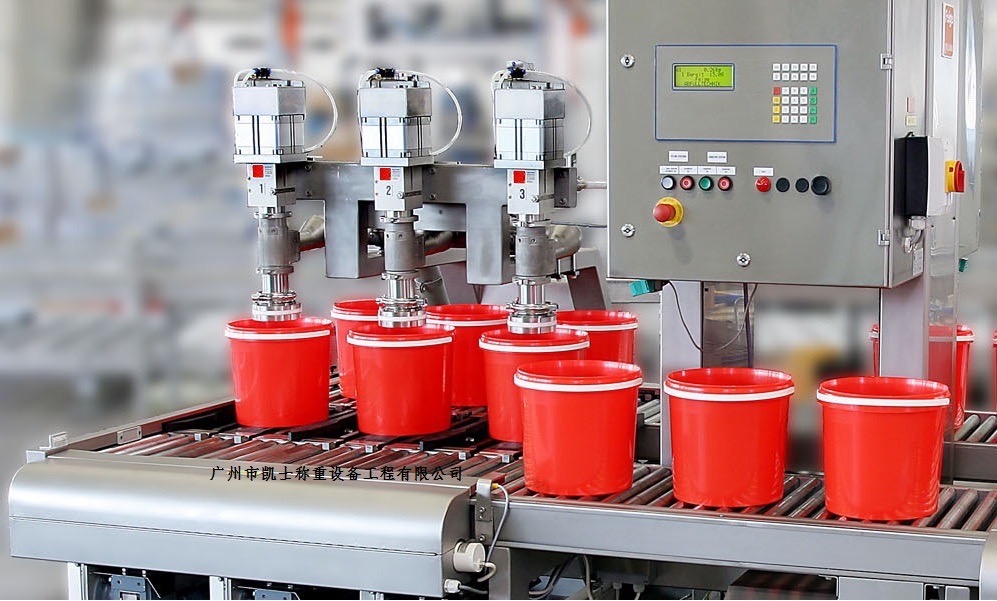
The tank liquid weigher achieves online measurement through an electronic weigher. Based on the detection results, the PLC controls the opening and closing of the solenoid valve, uses the separated oil liquid for weight compensation to achieve precise measurement. After the online measurement is completed, there are photoelectric sensors to count the already filled containers. The count is displayed on the operation display panel (touch screen). The conveyor belt then discharges the filled containers and the automatic filling process is completed.

 020-34563445
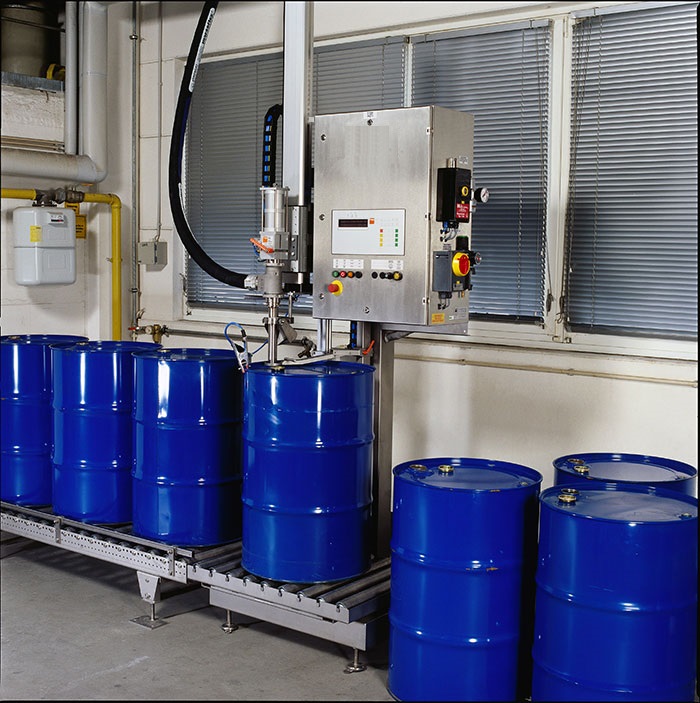
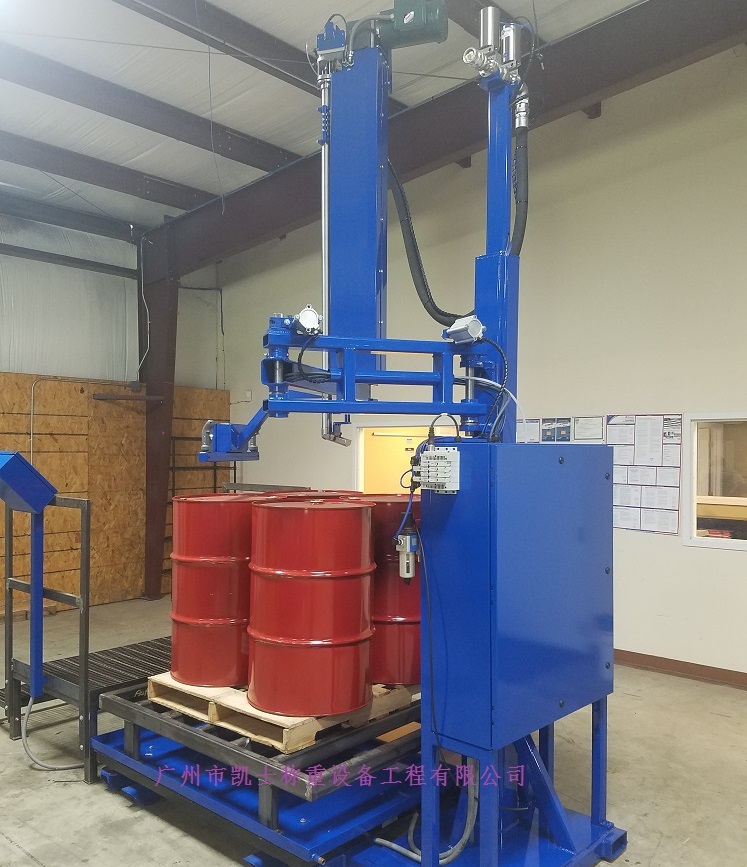
The filling weighbridge uses an electronic weighing platform controlled by a PLC program for measurement. It integrates mechanical, electrical and instrumentation components, and is a filling equipment that combines weighing and filling functions. During filling, the system automatically removes the empty weight first. When the material is injected into the container, it is filled in a large volume and rapid manner first, and then the measurement is corrected slowly and in small doses. The operator only needs to place the container on the platform, align the bucket opening with the filling nozzle. At this point, the program starts, the filling nozzle automatically descends, and the filling valve is opened to supply the material. When the set quantity is reached, the filling stops automatically, the filling nozzle rises, and the filling process is completed. The quantitative weighing filling weighbridge is sent to the preparation hopper by the feeding mechanism, and the preparation hopper takes a three-material rapid delivery method to the filling gun, that is, the large, medium and small materials are unloaded to the filling bucket after completing the quantitative weighing in the filling gun. The entire quantitative process is controlled by the quantitative weighing instrument, and this controller also provides control for clamping the bucket and releasing the bucket.
The quantitative weighing filling port is equipped with a photoelectric sensor to detect whether there is an empty bucket. When the empty bucket rotates to the filling port, the rotating device stops, and the photoelectric sensor will feedback the detection signal to the PLC controller. The PLC will control the opening and closing of the solenoid valve based on the detection signal. The Electronic scale recognizes the opening of the electromagnetic valve for the empty bucket and fills the material into the bucket. After filling, the PLC controls the solenoid valve to close, and at the same time, the filling gun returns to the position. The conveyor belt realizes the transportation of the material buckets and achieves the online repeated weight detection of the material during the transportation process. The conveyor belt is driven by a stepper motor, and through the PLC control system, the step gap stops, and the electronic scale realizes online measurement. Based on the detection results, the PLC controls the opening and closing of the solenoid valve, uses the separated oil liquid for weight compensation, and achieves precise measurement. After the online measurement is completed, the photoelectric sensor counts the filled material buckets on the display panel (touch screen), and displays the count. The conveyor belt will send the filled material buckets out and complete the automatic filling process. During the entire filling process, it is required that the filling action time be equal to the step gap stop time of the conveyor belt and the intermittent mechanism's intermittent stop time. The online weight compensation time should not exceed the stop time.