


















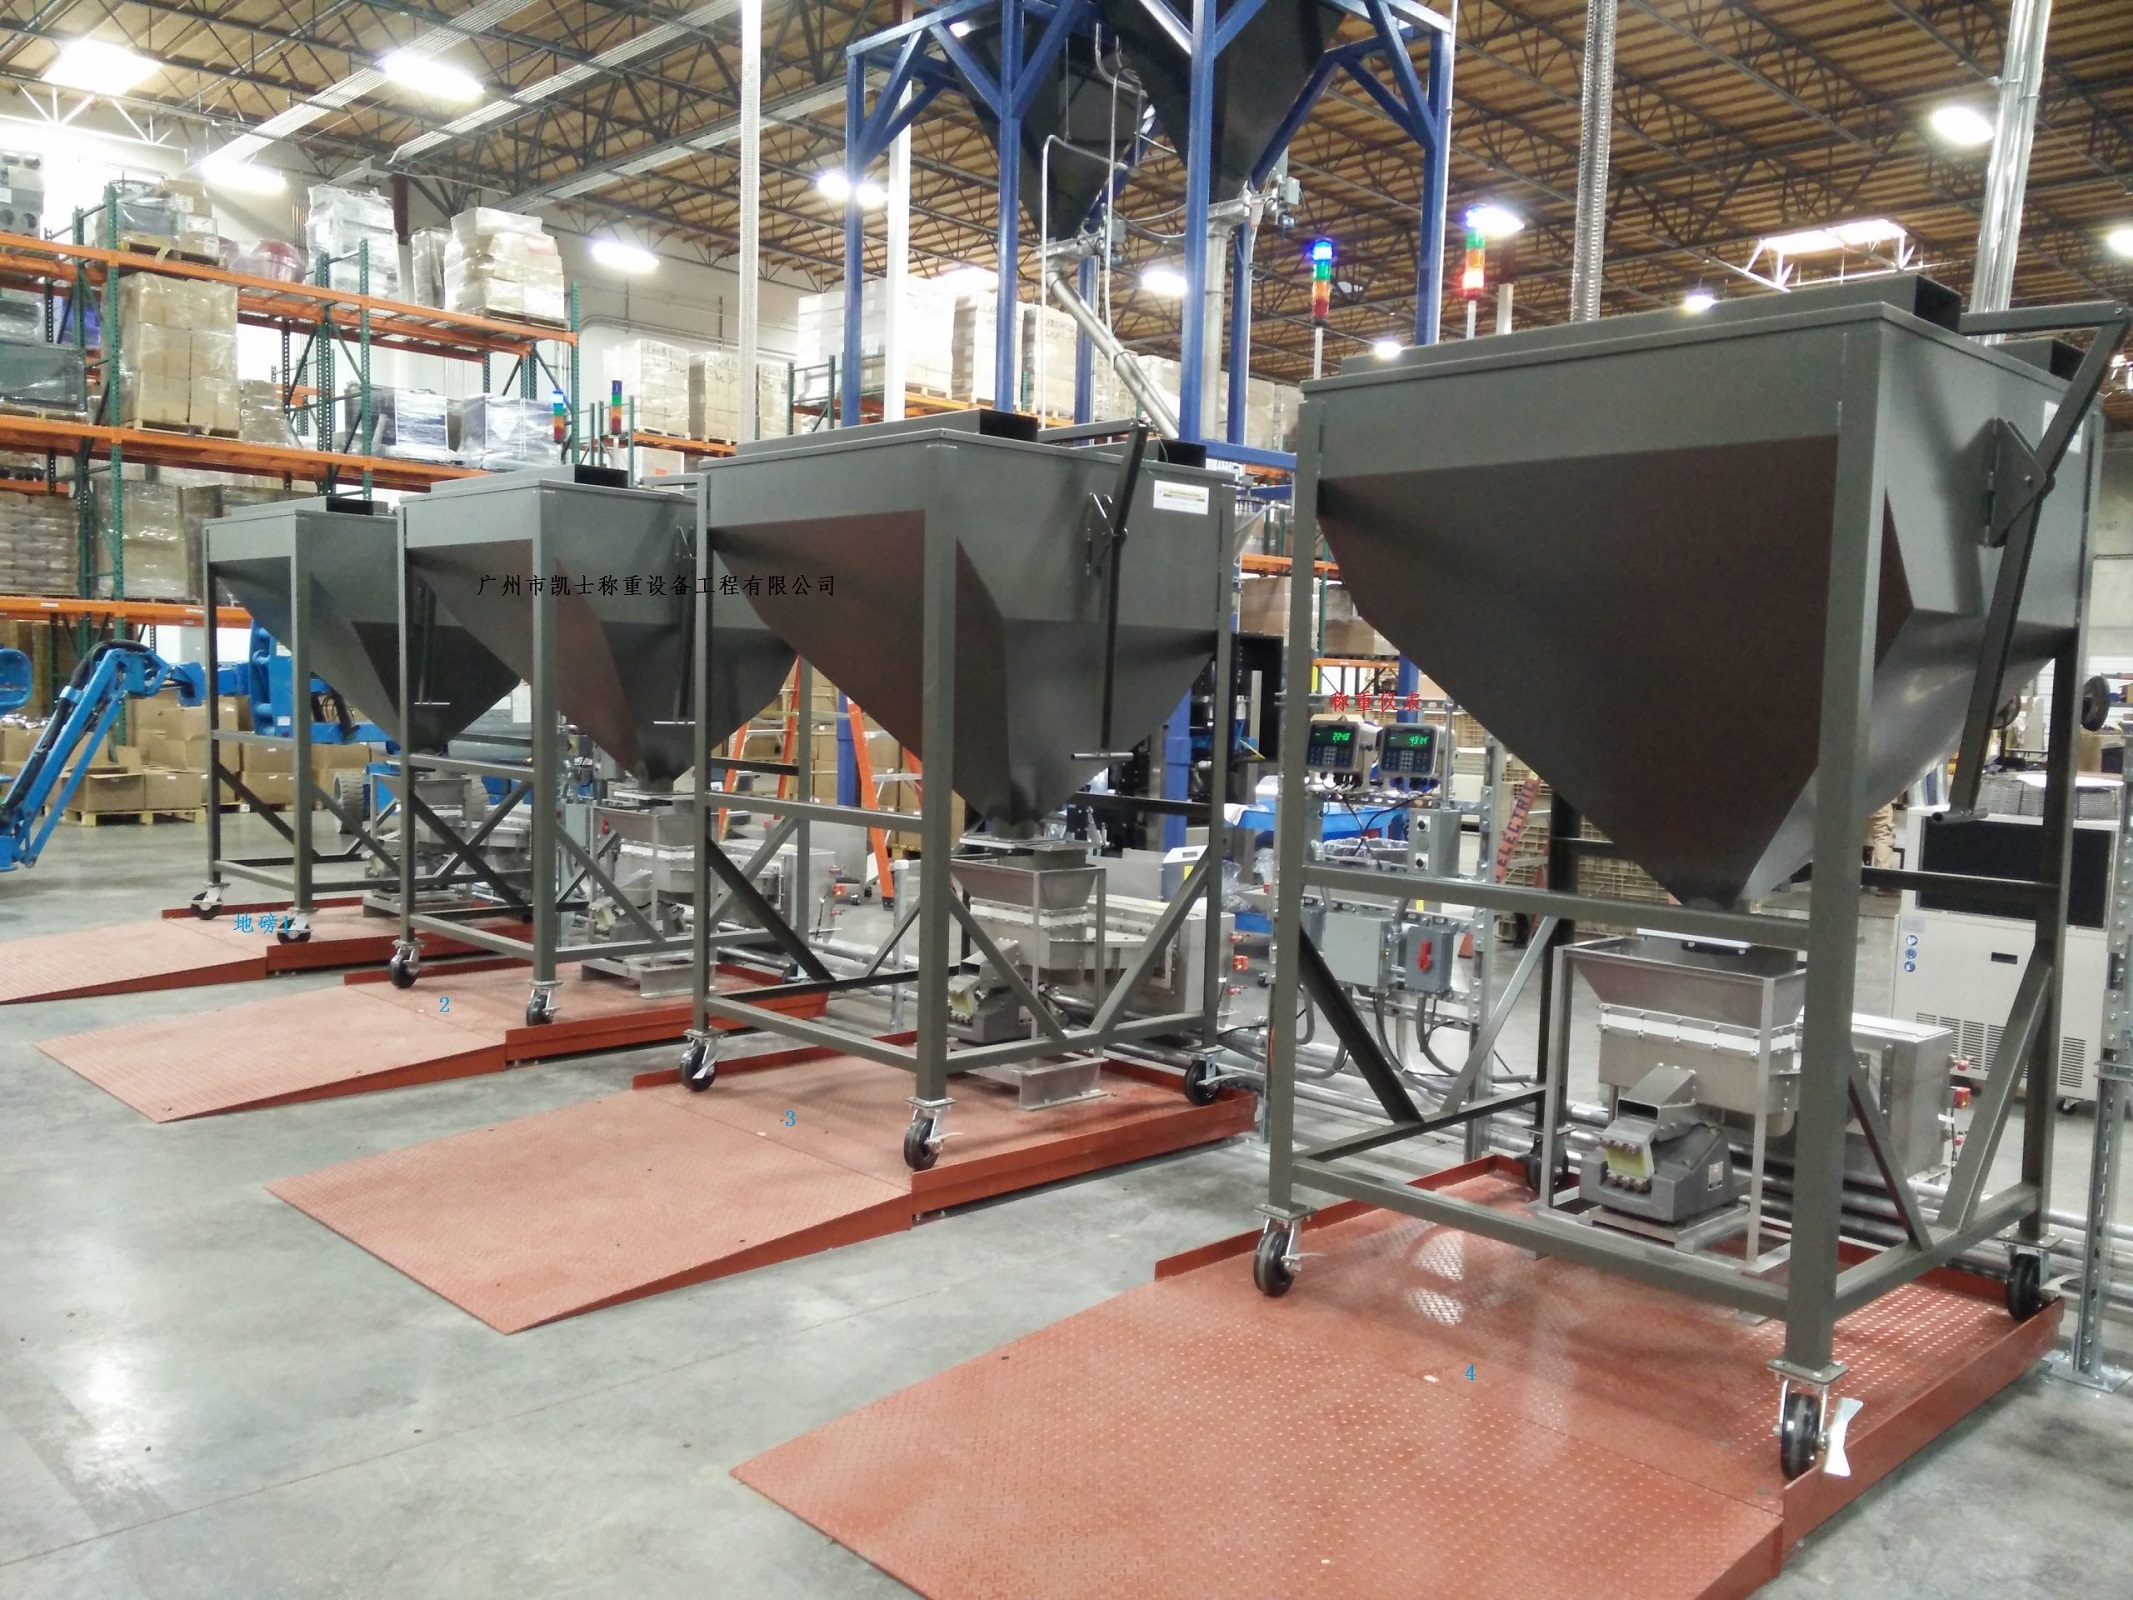
TheExplosion-proof feeding scale uses a frequency converter to achieve two-speed speed control for feeding, thereby realizing the functions of fast, slow and point feeding control for four types of materials, ensuring the accuracy and speed of variable-frequency feeding. After starting the pre-set metering feeding program, the weight of the hopper conveyor belt is measured and stored, and then various ingredients are successively controlled to enter the hopper conveyor. Among them, dry materials are metered into the hopper conveyor by a vibrating disc, powder materials are metered into the hopper conveyor by a screw feeder, liquid materials are metered into the hopper conveyor by a hydraulic valve, and pasty materials are metered into the hopper conveyor by a pump.

 020-34563445
The explosion-proof feeding scale is a production equipment used in industry for automatically and precisely proportioning different powders or materials in a certain ratio for processing. It is usually composed of a Weighing system, weighing instrument, PLC system and upper computer. The explosion-proof scale includes various equipment such as raw material storage body, conveying body, electronic platform scale, dust removal body, material mixing body, etc.; it consists of two parts: main circuit and PLC system. The components are pumped into the hopper scale through the rotor valve and injected into the mixing hopper by itself, and the self-weight acts on the Electronic scale. When the electronic scale is subjected to force, its 0-10V output voltage signal is sent to the A/D converter (weighing instrument), converted into a digital signal and sent to the PLC for processing. The control values of various components have been input to the PLC through HMI. The PLC sends the detected weight value to HMI for display and comparison with the given value. When the detected value is equal to (or greater than) the given value, the control interface outputs a control signal to stop the pneumatic valve from adding ingredients and complete the addition of the first raw material. Then, the second raw material is added, and other raw materials are added in sequence. After all ingredients are added, the PLC sends a signal for stirring, and the stirring time is set by HMI and sent to the PLC. After stirring, the materials are automatically placed in the hoppers on the scale platform.
According to the control function requirements of the electronic scale, various logical, sequential and process controls need to be carried out for the equipment, including manual and automatic control of the equipment, various alarm inputs, outputs and signal feedback, etc. This requires more PLC input and output points. The input signals controlled by PLC include the start-stop buttons on the scale operation panel, the upper and lower limit of the level switch, the signal indicating that the pneumatic valve is closed in place, the overload signals of each motor, etc.; the output signals controlled by PLC include: the operation status indication of each motor and electromagnetic valve, the intermediate relay AC contactor of the discharge valve and other contacts. During the operation of the scale system, users need to input relevant information such as the number of the hopper and the formula of the surface layer, the mixing hopper, the limit control values of the surface layer hopper and the feeding time, and print the per-minute weighing data and the historical curve of the surface layer material consumption. According to these requirements, the PLC is connected to the human-machine interface (HMI) via RS-485, and the HMI is connected to the micro printer via the USB interface. The on-site switch signals directly enter the input port of the PLC, while the hoppers on the scale platform, the weight signals of the scale and the hoppers are from the analog acquisition module and enter the PLC. For the control signals output by the split PLC, 24V signals are divided into one group and shared with the positive pole, directly connected to the actuator through the PLC; 220V feeding pumps and mixers are divided into one group and also controlled directly by the PLC. The HMI is a bridge for two-way communication between the operator and the machine equipment. Operators can input data according to the prompts on the screen, observe the changes in process parameters, monitor the production process in real time, achieve visual operation, and reduce operational errors. The HMI is also responsible for downloading the parameter values of the material mixing process to the PLC and printing out real-time data at the end of the process.
The electronic scale uses a frequency converter to control the feeding at two speed levels, thereby achieving the functions of fast, slow and point control for four types of materials, ensuring the accuracy and speed of variable frequency feeding. After starting the pre-set metering feeding program, the weight of the hopper machine is measured and stored, and then various ingredients are controlled to enter the hopper machine in sequence. Dry materials are metered and fed by a vibrating disc, powder materials are fed by a screw Feeder, liquid materials are fed by a hydraulic valve, and paste materials are fed by a pump. Each ingredient is successively fed using two feeding methods of coarse and fine materials to ensure a weighing accuracy of 98% - 99%. The weight of the materials is converted from the weighing instruments corresponding to the 3 electronic floor scales installed on the support frame and suspending the hopper machine into electrical signals. These signals are then converted into digital form and read into the PLC for weight calculation. After removing the tare weight, it is compared with the set value. The result serves as the basis for controlling the material switching or the conversion between coarse and fine feed. The mixed substances that have completed the weighing are discharged through the valve into the heated hopper, where they are stirred. Then, they are pumped into the container and enter the packaging process.


