
















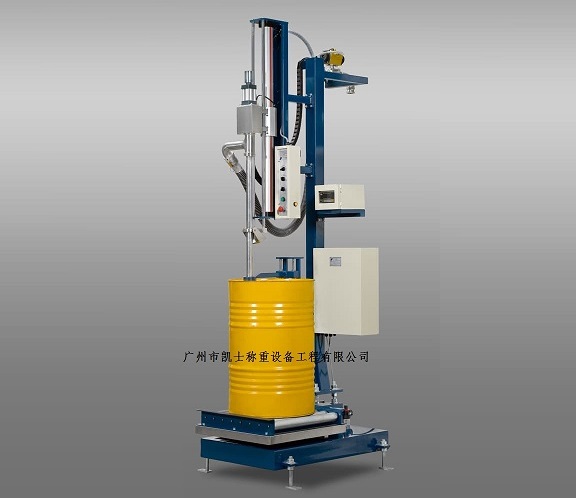
The Liquid medicine automatic filling machine adopts a number of core patented technologies, such as machine vision dynamic target recognition technology, intelligent filling process control and detection technology, composite explosion-proof technology, fault self-diagnosis and self-processing technology, Internet of Things (IOT)-based leakage detection technology, and so on; the products are all characterized by advanced technology, excellent quality, safety and environmental protection.

 020-34563445
The automatic liquid medicine Filling machine adopts a controller with bus communication function, and the software platform has developed a filling control management system through SOL+WINCC software. The Filling system utilizes industrial control computers to achieve monitoring and control functions, and implements process and equipment control signals such as toxic and harmful gas probe signals, liquid level, pressure, mixing, current signals, pump and other facility status, start stop and other equipment data through programming software to form causal conditions with the filling system process, realizing logical interlocking control. The entire control system is equipped with four UPS power supply devices to ensure stable and reliable system operation. The filling machine adopts intelligent design, and the entire filling system is divided into 3 sub packaging filling lines, 1 set of PLC system, and related software and hardware systems. Touch screen devices are configured in each production line to achieve unit control of each control link, and to timely track the function and working status displayed separately on site. The weighing and measuring part used on site is managed by two sets of bus communication functions and an independent PLC system. The Liquid filling machine operates under the drive of a servo motor; One side of the filling rack is adjacent to one end of the first conveyor device; The feeding mechanism is set on the filling rack, and the new metering filling machine adds two types of medicinal liquids separately to achieve mixing of the medicinal liquids. The feeding mechanism includes a feeding box, a first feeding head, a second feeding head, and a canning tube, and the feeding box is set on the filling rack; The first feeding head and the second feeding head are arranged opposite each other on the feeding box, and the canning tube is connected to the feeding box. The first and second feeding heads need to be as close as possible to the upper edge of the filling barrel; In addition, the first feeding head is equipped with a coarse feeding valve and a fine feeding valve. During feeding, the coarse feeding valve is opened under the control of the control device to quickly feed the material. When the set value is reached, the coarse feeding valve is closed and the fine feeding valve is opened for fine feeding; Coarse feeding can achieve fast and rapid feeding, while fine feeding can better ensure the accuracy of feeding, thereby improving the overall filling efficiency. In addition, the structure of the second feeding head is the same as that of the first feeding head. In order to better control and prevent debris from entering the material bucket, a filtering device is installed between the feeding mechanism and the receiving device. The filtering device filters the debris in the liquid medicine discharged through the canning tube to prevent the mixture of debris and the liquid medicine from being filled. The filtering device is a filter screen; Due to the addition of liquid medicine in the feeding box, a float is set up, which is installed on the feeding box; By observing the position of the float, the liquid level in the feeding box can be obtained to avoid excessive feeding; During the process of liquid filling, the liquid (liquid) has viscosity. Even after the feeding mechanism is closed, the liquid still sticks to the outlet of the feeding mechanism and slowly drips, causing the liquid on the outlet of the feeding mechanism to drip onto the first conveying device, the first carbon steel weighbridge, or the second double-layer weighbridge. The receiving device is set on the filling rack and located at the lower part of the feeding mechanism; When filling, separate the feeding device from the filling rack. After filling is completed, reset it, and then use the feeding device to collect the dripping adhesive medicine at the outlet of the feeding mechanism. The feeding device is set on the bracket of the filling rack, and the feeding device is preferably a tray. When feeding, the tray is placed on the bracket, and when filling, the tray is removed;
The weighing and filling machine is installed on the filling rack with the first waterproof weighing scale and the second stainless steel weighing scale, and is adjacent to one end of the first conveyor device; The material buckets transported by the first conveying device are placed on the first buffer weighing scale and the second material bucket weighing scale, respectively. Two material buckets can be set on the first tank material weighing scale and the second formula weighing scale at the same time, and the liquid medicine passing through the receiving device is placed in the material buckets respectively. The weight of the material buckets is measured in real time by the first filling weighing scale and the second filling weighing scale. When the set value is reached, the filling is stopped, and the material buckets enter the next stage. The control device is adjacent to the filling rack and is connected to the first feeding head, second feeding head, canning tube, first filling weighing scale, and second filling weighing scale of the first conveying device. On the one hand, it inputs control instructions, and on the other hand, it monitors the status of each part in real time. When the set value is reached, it stops responding to component actions; PLC adjusts the working status of each part by setting data for the system; The control device can also be a computer, specifically a component that can achieve control and monitoring. In order to provide better prompts, an alarm device is set up, which is connected to the control device. When a component has a problem, the control device will send the information to the alarm device for alarm. The alarm device is a sound and light alarm; In order to improve overall efficiency and reduce manual labor, the automatic filling machine is equipped with a second conveyor and a top cover device, which are adjacent to the other side of the filling rack; The upper cover device is set on the second conveying device, and the barrel containing the medicine conveyed by the second conveying device is covered by the upper cover device; That is, the material bucket lid is automatically covered by an upper lid device, which includes an upper lid frame, a lid holding device, a lid supporting device, a lid taking device, and a rotating device. The upper lid frame is set on the second conveyor device; The cover holding device is set on the upper cover frame; The support cover device is set on the upper cover frame and placed below the holding cover device, and the cover removal device is set on the upper cover frame and placed below the support cover device; The rotating device is set on the upper cover frame; The quantitative filling machine places the bucket lid on the lid device. Due to the presence of several limit rods on the upper lid frame, which cooperate with the lid support device to limit the position of the bucket, when the lid is removed through the lid removal device, the second to last bucket lid below will be clamped by the lid removal device to prevent it from being removed together with the last bucket lid. The lid removal device consists of several lid removal cylinders set on the upper lid frame and lid removal blocks set on the lid removal cylinders. The movement of the lid removal blocks is controlled by the action of the lid removal cylinders, thereby achieving the clamping action of the bucket lid.
The automatic filling machine also uses a cap support device to lift the edge of the barrel cap through a cap support cylinder. When the cap is removed through the cap removal device, the cap support cylinder shrinks, which does not affect the cap removal device's ability to extract the barrel cap; In addition, the cap removal device includes a first suction cup and a second suction cup that are relatively arranged on the cap removal cylinder. Under the control of the rotating device, the cap removal cylinder drives the first suction cup and the second suction cup to rotate, and then uses the first suction cup and the second suction cup to respectively suck up the bucket cap. The rotating device is a linear motor connected to a rack, and the cap removal cylinder is connected to the upper cap frame through a bearing, which is provided with teeth that are compatible with the rack. In this way, under the driving of the linear motor, the cap removal device rotates through the meshing of the rack and teeth; During use, due to the fully automatic operation, there may be situations where the bucket lid is not in place. A missing lid detection device is installed, which is mounted on the lid support device; In this way, when the lid of the barrel reaches the corresponding position in a certain stage, it will be detected by the missing lid detection device and an alarm will be triggered, which can be sounded by an audible and visual alarm; To achieve automated processing, a capping device is installed, which is located on the second conveyor and adjacent to the upper cover device; When the lid of the barrel is placed on the medicine barrel through the upper cover device and further conveyed through the second conveying device 9 to reach the capping device, and the lid is pressed against the medicine barrel through the capping device, the capping device includes a capping frame and a capping part, and the capping frame is set on the second conveying device; The capping part is set on the capping frame; The measuring filling machine includes a capping group in the capping part, which is set on a locking plate on the pressing frame, and the locking plate is connected to the capping frame in a movable manner. The position is adjusted under the driving of the screw set on the capping frame to perform capping on barrels of different sizes; The cover group includes a compression cylinder, and a connecting column connected to one end of the compression cylinder; The two ends of the connecting column are connected to the pressing plate through a pressure cover plate; When the bucket that has been covered by the upper cover device is transported to the lower part of the capping device, the capping cylinder moves to drive the connecting column to press the pressure, thereby achieving the capping of the bucket. Of course, in the process of capping, it is necessary to avoid the displacement of the barrel lid and prevent external contact with the capping device. A pressure protection device is installed on the pressing frame to prevent external contact with the capping device while avoiding displacement.
Basic Parameters:
Maximum weighing capacity: 300kg
Minimum sensitivity: 0.1kg
Filling error: ± 0.1-0.2kg
Filling speed: 200L, approximately 50-80 barrels per hour
Control mode: 2nd gear control
Filling method: Insertion type, above liquid level
Gun head pipeline: PTFE gun head, valve+PTFE hose
Structural material: SUS304 stainless steel for the host, carbon steel for conveying and stacking with anti-corrosion paint.
Scale platform size: 800 × 800mm (304 stainless steel power raceway)
Empty bucket raceway: 800mm × 2500mm (304 stainless steel power raceway) with an additional 1200mm sloping unpowered drum
Heavy bucket raceway: 800mm × 2500mm (304 stainless steel power raceway, 2 sets)
Bucket sorting device: suitable for 20L buckets, carbon steel anti-corrosion paint structure, 304 stainless steel raceway.
Stacking equipment: translation type, suitable for pallets of 1200 × 1200 × 140mm, including pallet supply, palletizing, and lower pallet conveying.
Pipeline pressure: 0.2-0.6MPa (depending on material properties).
Material interface: 4 DN40 flange joints, available according to user provided interface standards
Air source interface: The user provides a 12mm air hose connector for quick connector connection
Power supply: AC220/50Hz (provided by the user to the machine side)
Gas source used: 0.4-0.8Mpa (provided by the user to one side of the machine)
Operating temperature: -10 ℃ -50 ℃
Basic conditions: A solid concrete floor with emulsifier and a concrete thickness greater than 10cm.
Optional models: Standard, Explosion proof Filling








