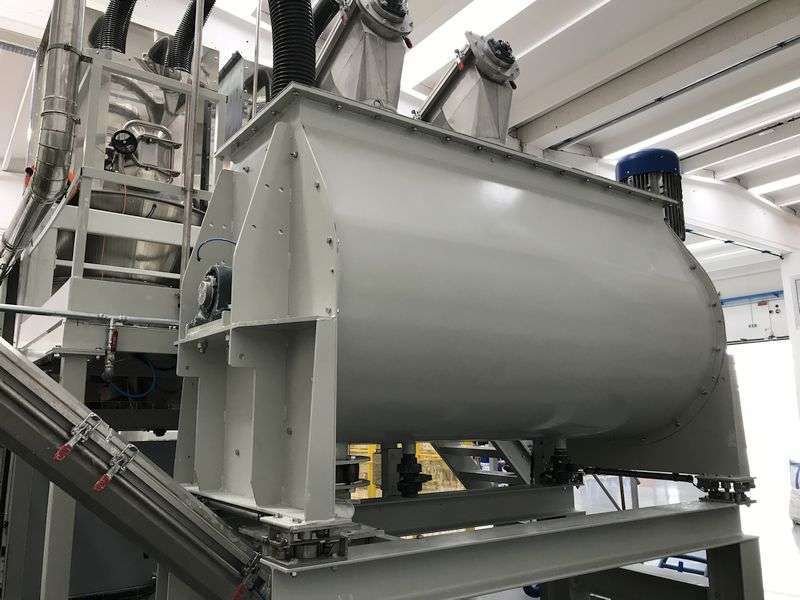
The Concentrated automatic dosing machine calculates the formula according to the detection data, and inputs it into the computer system through the man-machine interface or computer network. The computer control system automatically calculates the supply ratio of each raw material according to the detection data and the process formula, and then the PLC control system synthesizes the supply speed of each raw material supply system to accurately and continuously complete the raw material ratio according to the process sequence.



 020-34563445
The automatic centralized batching machine is guided by the principles of centralized control and decentralized management. The structure of the upper and lower computers is composed of computers and PLCs to achieve the system control objectives. The hardware part includes the selection of upper computer design, lower computer design, and communication hardware design. Siemens S7-200 series PLC was selected, which can meet the control requirements well in terms of reliability. Wireless communication equipment was chosen as the communication hardware, and STEP7 Micro/WIN32 programming software was used as the development tool for software design. The feeding part is the actuator that feeds the weighing equipment from the silo, using electromagnetic vibration Feeder, screw feeder, and dual speed solenoid valve; The weighing section consists of Weighing modules, standard connecting components, junction boxes, and hopper scales, which are used together with weighing instruments to weigh materials and detect errors; The discharge equipment consists of an exhaust valve, an electromagnetic vibration feeder, and an electrical vibration valve; The ingredient control system consists of weighing instruments, upper level control machines, CRT display devices, programmable controllers, wireless communication devices, and other control components; The ingredient weighing module should be regularly calibrated to ensure the accuracy of the system's ingredients.
The weighing and batching machine adopts a hopper weighing device. The bottom of the hopper is fixedly connected to a support frame, and the bottom of the support frame is fixedly connected to a bracket. The bottom of the bracket is fixedly connected to a base, and the top of the base is fixedly installed with a telescopic rod. A limit support rod is fixedly installed at the top of the hopper between the two telescopic rods, and the outer movable sleeve of the limit support rod is connected with a spring. The top of the limit support rod is fixedly connected with a weighing module, and the top of the telescopic rod is fixedly connected with a support crossbar. The top of the support crossbar is fixedly installed with a shaft socket, and the top of the two shaft sockets is fixedly connected with a shaft socket. The top of the left shaft socket is slidably connected with a sliding plate, and the top of the sliding plate is fixedly connected with a hopper scale. The right side of the hopper scale is connected with a The bottom activity connection has a compartment door, The two sides of the shaft seat are respectively provided with shaft grooves, and limited position springs are installed inside the shaft grooves. One end of the two limit springs near the outer side is fixedly connected to the shaft. The bottom of the right end of the hopper scale is fixedly installed with a spring installation tube, and the internal movable connection of the spring installation tube is a compression spring. The top of the compression spring is fixedly connected to the compartment door limit block, and the bottom of the compartment door limit block is fixedly connected with a connecting rope. The top of the right end of the base is fixedly installed with a feeding bin, and the bottom of the hopper scale is installed with a floor scale fixing sleeve. The middle of the support frame surrounds a square frame on the outside of the hopper. The support frame is made of steel structure, and the bottom of the hopper is supported by an Electronic scale support frame. There are four brackets installed at the bottom of the support frame. The telescopic rod is a hydraulic telescopic rod, which is divided into two stages. The spring is a reset spring, and the diameter of the spring is smaller than the bottom diameter of the weighing module. The telescopic support rod of the limit support rod. The weighing module is equipped with a weighing sensor inside, and the top diameter of the weighing module is equal to the inner diameter of the bottom fixed socket, which is located at the center of the hopper scale.
The weighing and batching machine shrinks two telescopic rods downwards to the bottom of the hopper scale, which is fixed on the outer side of the top of the weighing module. Continuing to shrink the telescopic rods, the shaft insertion seat at the top of the two telescopic rods is detached from the shaft seat at the bottom of the hopper scale, so that the hopper scale is completely placed on the top of the shaft. The overall weight of the hopper scale is recorded by the weighing module to complete the weighing operation of the ingredients. After weighing is completed, the two telescopic rods are lifted until the hopper scale is detached from the weighing module, and then the lifting of the right telescopic rod is stopped. The left side of the hopper scale is continued to be lifted by the left telescopic rod, so that the bottom of the hopper scale rotates around the right shaft seat, thus completing the rapid and thorough dumping of the concrete ingredients after weighing. The effect of quickly and thoroughly pouring the ingredients after weighing is completed. The weighing and batching machine uses a fixed length of connecting rope. When the telescopic rod lifts the hopper scale up to a certain height, the connecting rope is straightened and pulled downwards to pull the compartment door limit block, causing the compression spring to contract. The compartment door limit block slides towards the inside of the spring installation tube, and shrinks to the bottom surface of the hopper scale. The outer side of the compartment door loses the limit of the compartment door limit block. The ingredients inside the hopper scale can be poured outward by squeezing the compartment door, thus achieving flexible control of the weighing compartment door of the weighing machine.
Control requirements
1) The automatic and manual control functions of the ingredient system are controlled by the operator entering material formulas and other control parameters from the keyboard to automatically complete the process control. Manual control mode is a step-by-step control method in which the operator inputs material formulas, other control parameters, and specific control requirements from the keyboard.
2) The wireless communication method (free port communication method) system adopts wireless communication method and free port communication method.
3) Equipment operation fault status alarm and alarm record query, monitoring software monitors the operation status of various actuators, can provide emergency response and alarm prompts for various faults, and quickly eliminate faults. At the same time, the flexible and versatile control methods of the system also provide convenience for fault handling
4) Automatic compensation function for feed drop value. It can automatically correct the weighing of airborne materials during the ingredient preparation process, improving the weighing accuracy.
5) Full process system operation status monitoring and display function. Dynamically display the material quality and the operating status of each actuator on the monitor.
6) Production management and report printing, this function is used for managing production (such as recipe management) and printing reports.