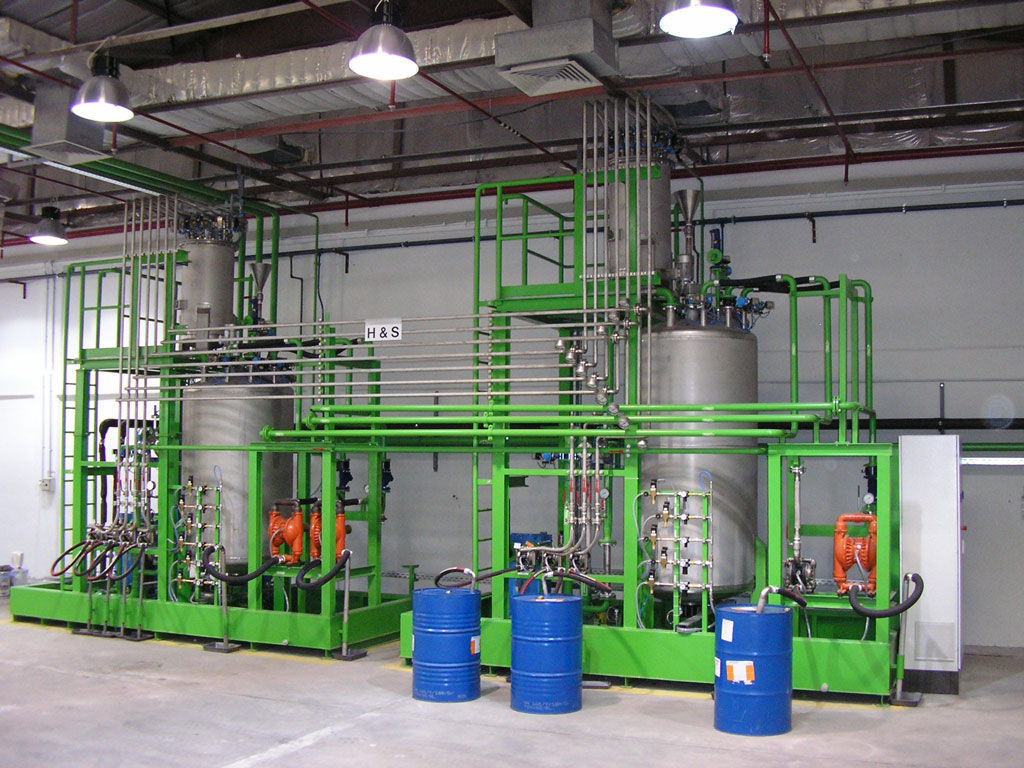
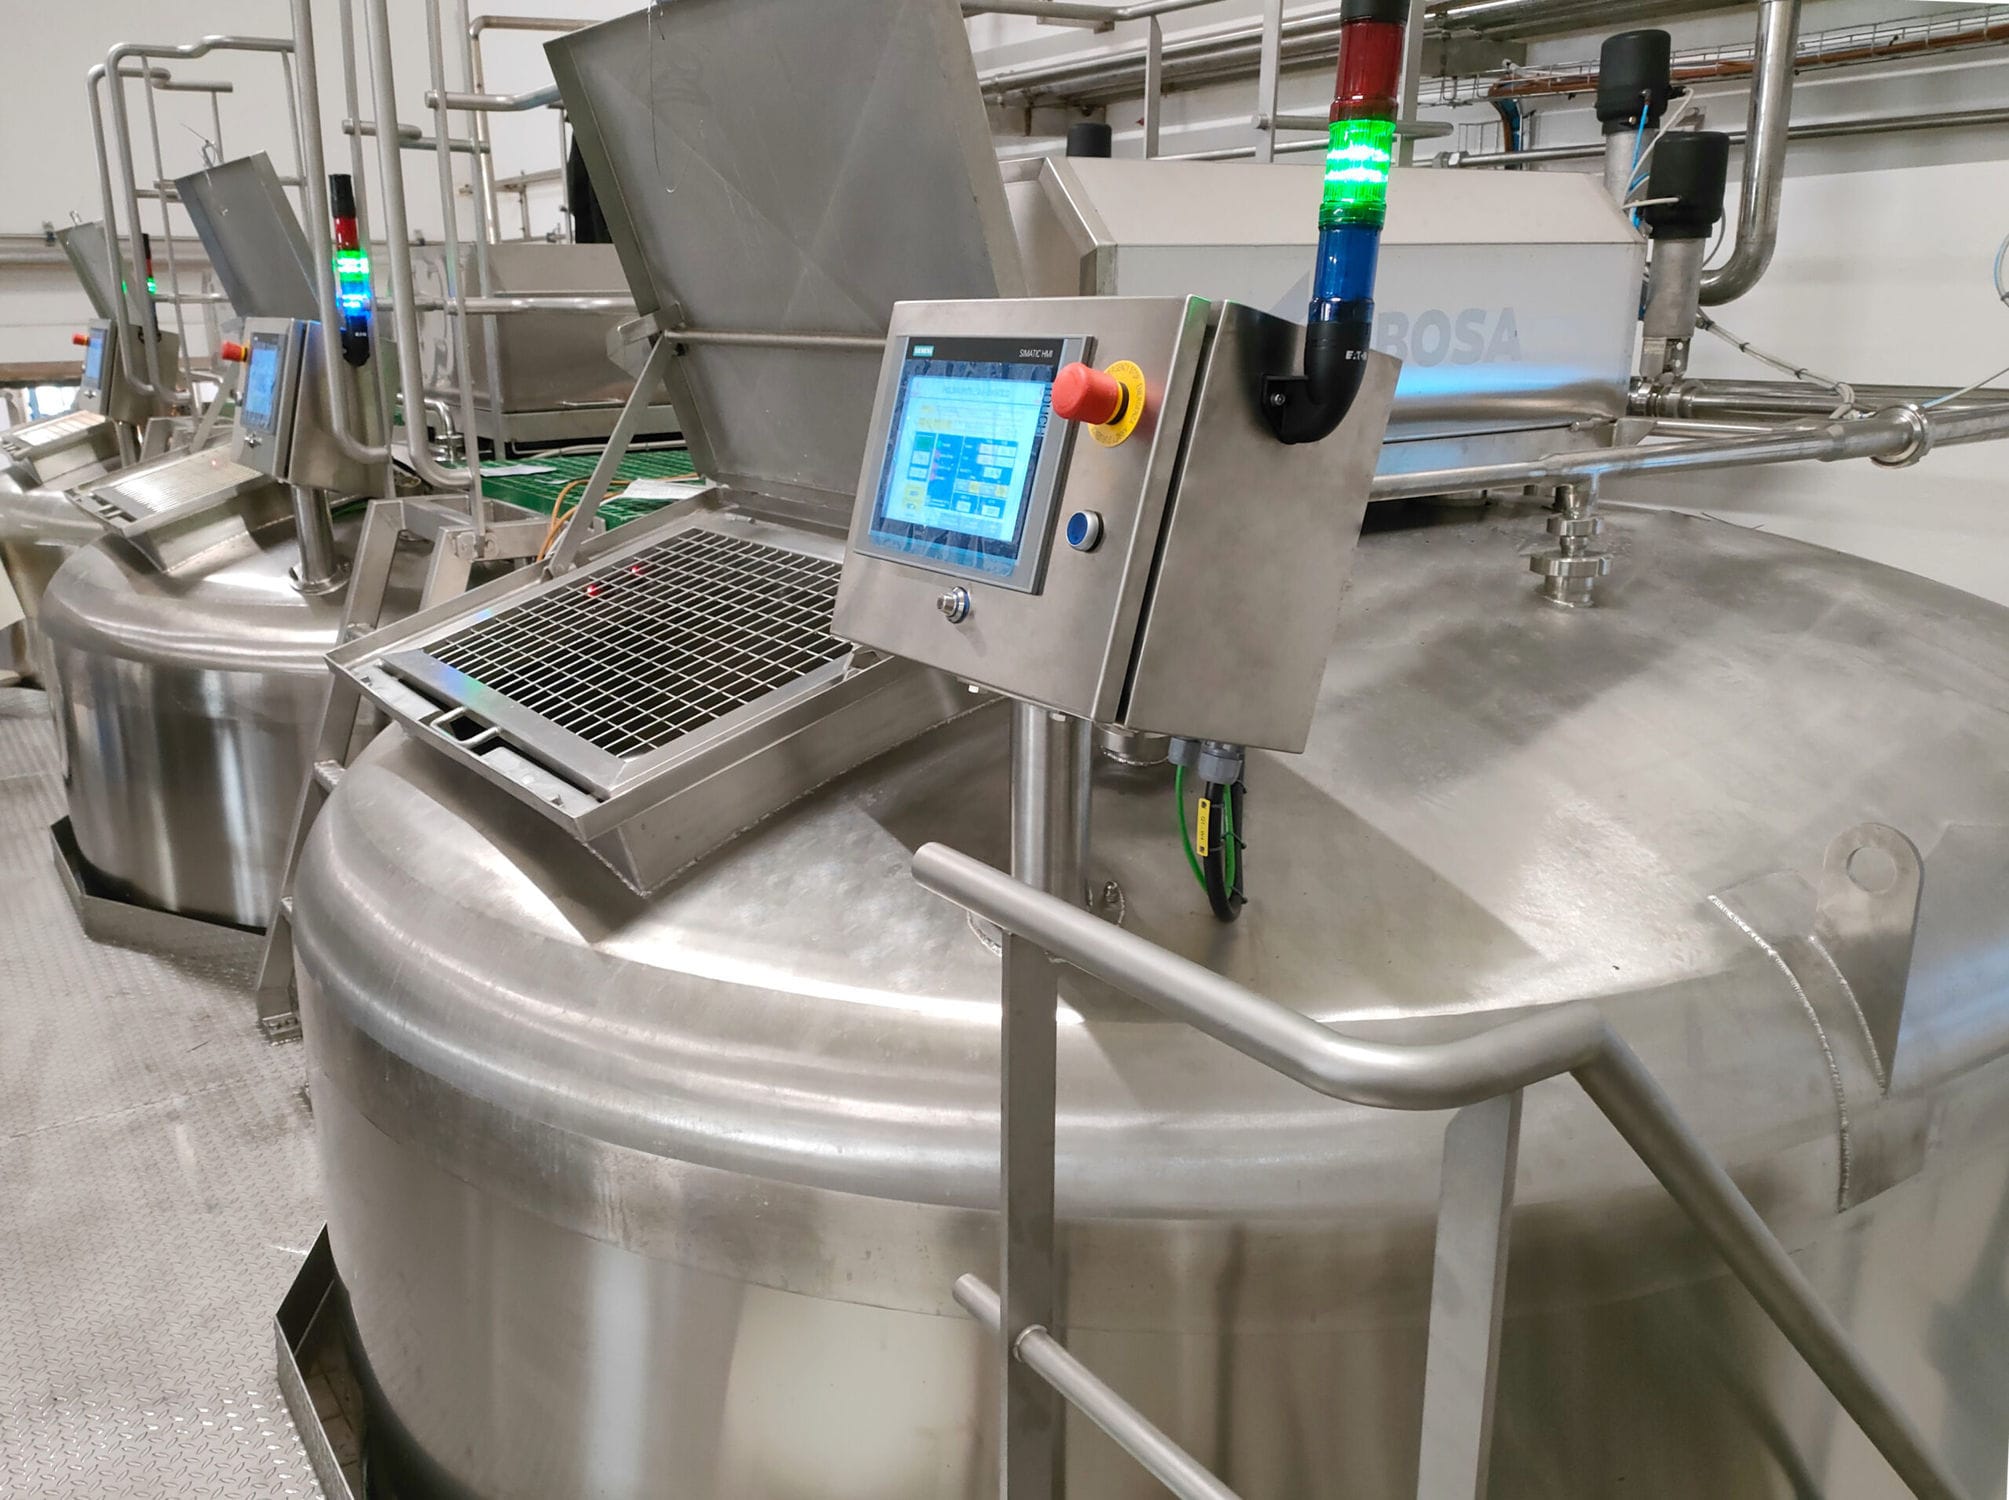
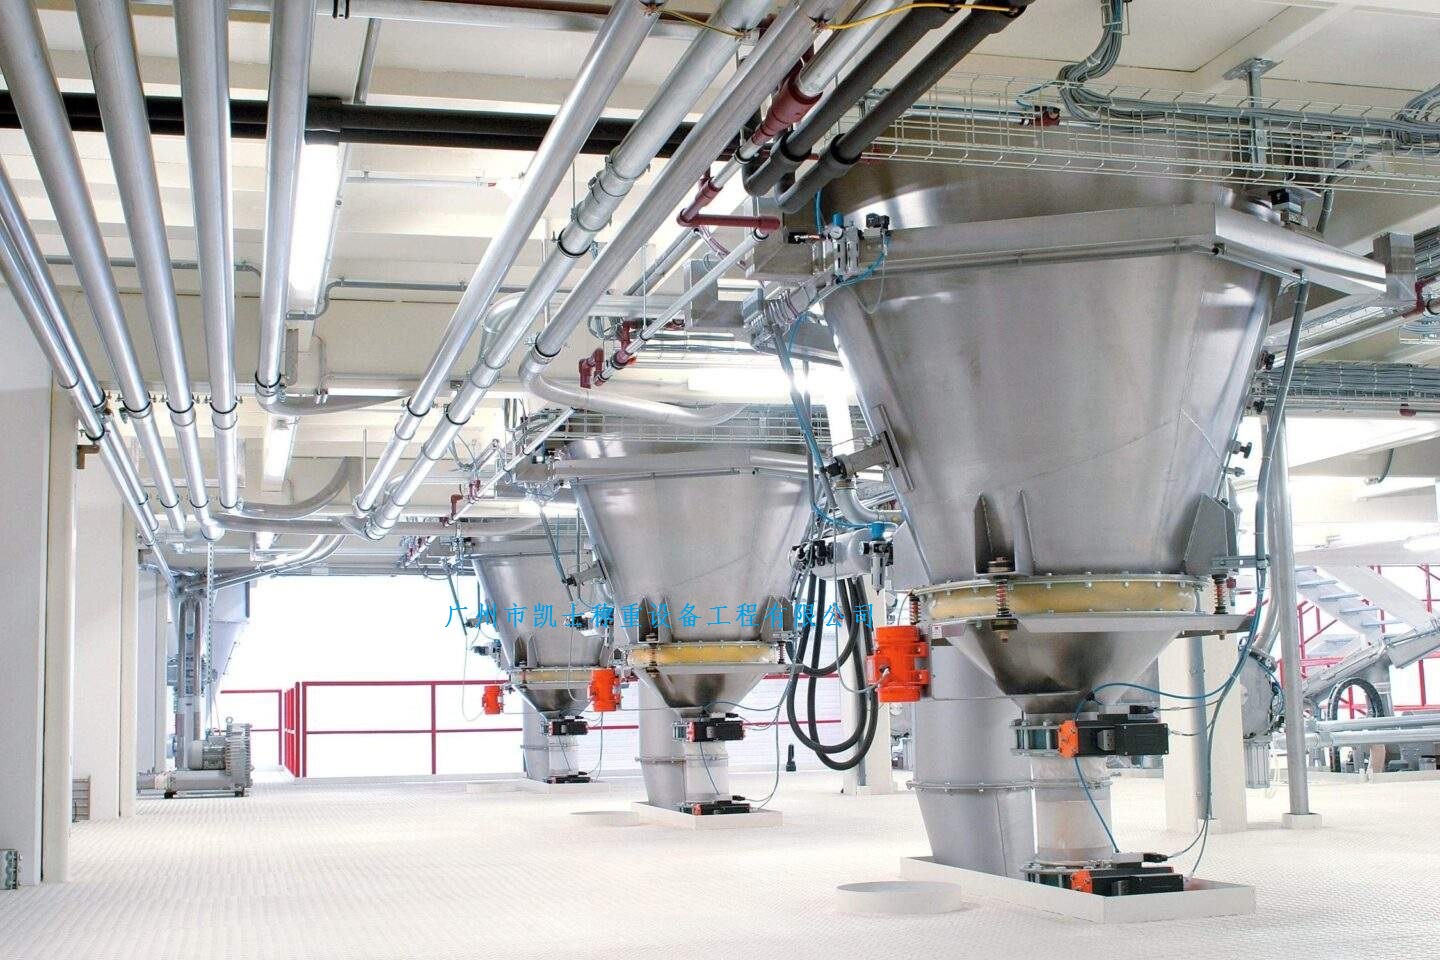
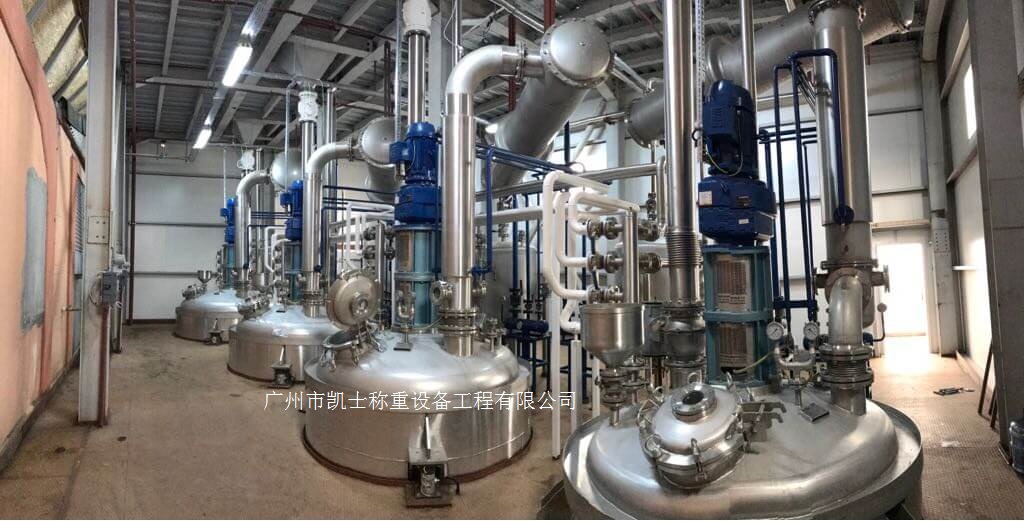
The feeding mechanism of the batching equipment is connected with the reactor, and the method of feeding two-speed feeding is adopted. When the weighing feeder stops feeding, part of the material falls into the weighing hopper in free fall in the air. The set value of the weight of the incremental method should be the standard weight value of the material to be formulated minus the drop value. By automatic weighing the bulk material according to the predetermined ratio, the weighing amount of the material can be controlled and the material can be discharged at the same time. When the material is completed, the pointer is moved to the corresponding proximity switch to make the action, and then the next step of material feeding and weighing is carried out, and so on until all the material ratio is complete.

 020-34563445
The batching hopper of the reaction kettle includes a hopper, and the lower half of the hopper is supported in a tapered cylindrical shape that gradually shrinks in a bracket. A turning valve is installed inward at the top of the hopper, and inlet and outlet ports that can be connected to the inside of the hopper are respectively provided at the outer ends of the turning valve. A pneumatic vibrator is installed on one side of the conical cylinder of the hopper with a fixed seat. A weighing module is installed at each support point between the hopper and the bracket, and the weighing module is electrically connected to the controller. A discharge valve is installed on the lower port of the conical cylinder of the hopper. There are 3-4 Weighing modules between the silo and the bracket. When feeding into the weighing silo, the turning valve cuts off the outlet channel and opens the inlet channel. The gas and material mixture being conveyed enters the silo through the inlet, and the material sinks into the silo under the action of gravity. The gas is discharged through the outlet channel of the silo, and when the weighing module reaches the set weighing standard, the output terminal of the weighing module sends an electrical signal to the controller. The controller controls the turning valve to cut off the outlet channel or open the inlet channel, closing the channel leading to the silo. The gas and material mixture flows directly from the inlet to the outlet and flows back, achieving the purpose of online weighing. When the discharge valve is opened for discharging, the vibrator is turned on to accelerate the discharge and prevent blockage.
During the entire operation of the feeding system, the temperature in the reaction tank is controlled within a certain range, and a temperature sensor is designed to control the jacket temperature. For industrial control computers, they collect and output signals from variables to achieve communication between the industrial control computer and the on-site reactor. The monitoring software is connected through an RS232/485 conversion module and can be adjusted according to the time required for the material to fully react. The reaction tank temperature jacket temperature cascade batching composed of computers and electric regulating valves, the selection of control methods and algorithms, the setting of set values and related parameters, and the display box of the real-time temperature control curve of the reaction tank enable the proportional coefficient and online debugging to intuitively adjust the integration time and differentiation time in a timely manner according to the shape of the real-time temperature curve inside the reaction tank, and obtain the full range.
The screw conveyor selects the feeding screw according to the material properties. The powder material properties mainly refer to the bulk density, fineness, moisture content, flowability, etc. It is composed of two screws that rotate in the same direction and mesh with each other. The screw edge is narrow and the groove is wide. During operation, the material is conveyed forward along the spiral in an ∞ - shaped channel. The screw tip of one screw can scrape off the material layer on the interface by stable tangential sliding against the side of another screw. Through the weighing module, the signal is transmitted to the weighing instrument, which changes the motor speed through a frequency converter to alter the feed flow rate. Due to the ability of the weighing sensor to constantly transmit changes in the material inside the machine to the weighing instrument, the material flow rate always fluctuates around the set value, resulting in high accuracy of the average feed flow rate. The screw conveyor is connected to the feeding mechanism and the reaction kettle, which can evenly control the transportation of materials from the reaction kettle. According to job requirements, material conveying and inclined conveying can be carried out. In the production process or technological process, the method of feeding with dual speed weighing is adopted. After the weighing Feeder stops feeding, a portion of the material falls freely into the hopper scale in the air. The set value for weighing materials using incremental method should be the standard weight value of the material to be prepared minus the drop value. By using automatic weighing to weigh bulk materials according to a predetermined ratio, the weighing of the materials can be controlled, and unloading can also be achieved. Unloading adopts the zero position method. When the material is completed, the pointer moves to the corresponding proximity switch to make the action, and then the next step of material feeding and weighing is executed, and so on until all materials are proportioned.