
















The Measurement reaction kettle industrial control system realizes the dosage control of the reaction kettle, the serial control of the temperature inside the reaction kettle and the jacket temperature. It includes creating real-time database, making process flow diagram and animation connection, designing operation strategy and window configuration. The control process is to create a script program component in the "Startup Strategy" of the MCGS "Operation Strategy" window, write a program to open all solenoid valves except the feed valve, start the timing tank with a 2-minute delay so that all tanks and reactors will be emptied at the beginning of the system operation, and set the cycle time for all tanks and reactors to be emptied at the beginning of the system operation. Set the period to 200 milliseconds, add a script program component to it, and write a control program based on the flowchart.

 020-34563445
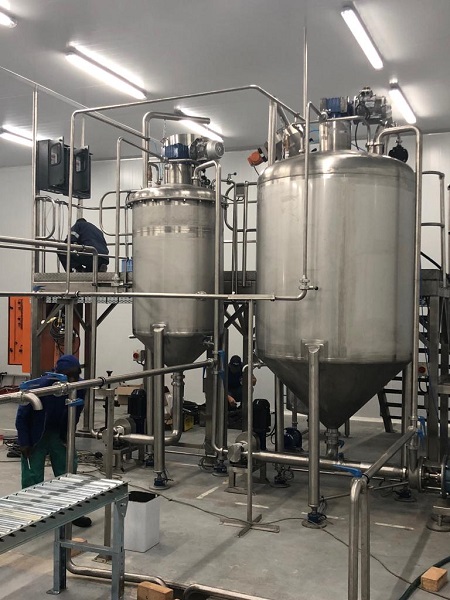
When installing reaction vessels and using weighing sensors, various issues such as load transfer, installation of connectors, and container deformation must be considered. The Electronic scale and other components are combined in the mixing kettle for measurement. The electronic scale can be easily connected to various shapes of mechanical devices to form a Weighing system, such as connecting rollers, platforms, vertical tanks, tanks, hoppers, reaction kettles, etc. The electronic scale has fully automatic, automatic, and manual functions. Regardless of the method, electronic scales always have a mandatory function. The function of electronic scale can immediately start or stop certain operations to cope with unexpected events, making the electronic scale system more adaptable. The reaction kettle weighing system starts the weighing instrument to track and read the weighing sensor signal. When the weight approaches the preset large feeding value, the instrument will turn off the fast feeding signal, allowing the system to enter the slow feeding process. At the same time, the instrument continues to track and read the weighing sensor signal at any time. The instrument automatically turns off the small feeding signal, stops the feeding process, and the measurement ends. The industrial control system of the measuring reaction kettle realizes the batching control of the reaction kettle, the cascade control of the temperature inside the reaction kettle and the jacket temperature. This includes creating real-time databases, creating process flow diagrams and animation connections, designing operational strategies, and configuring windows. The control process involves establishing script program components in the "Start Strategy" section of the MCGS "Run Strategy" window, writing programs, opening all solenoid valves except for the feed valve, delaying the start of the timing tank by 2 minutes to clear all storage tanks and reaction tanks at the beginning of system operation, setting the cycle to 200 milliseconds, adding script program components to it, and writing control programs according to the flowchart.
The weighing of the reaction kettle connects different material bins to each feeding branch pipeline, and calculates the weight of each material to be weighed in advance. When one of the materials is weighed, the solenoid valve set on the feeding branch pipeline connected to that material is opened, and the solenoid valves set on the other feeding branch pipelines are closed. Vacuum is drawn through the vacuum pipeline, making the conical hopper negative pressure. Under the action of negative pressure, the material passes through the feeding main pipeline to the feeding branch pipeline and then to the conical hopper. During the process of the material falling into the conical hopper, the weight weighing module set on the conical hopper weighs and measures the material. The principle of weighing other materials is the same as above. After weighing is completed, the vacuum in the conical hopper is discharged through the exhaust port, and the plug-in valve is opened to dispense the material. Good materials can be taken out, and a mixing device can also be installed in the conical hopper, Realize the mixing function during the weighing and batching process. By connecting the feed main pipeline to the conical hopper, and then connecting the manager branch pipeline on the feed main pipeline, each feed branch pipeline is controlled by an electromagnetic valve, which can achieve automatic weighing and batching of various materials. Setting a filter in the buffer section can avoid problems such as vacuum pipeline blockage and pollution caused by materials entering the vacuum pipeline during vacuum suction. The pulse motor connected to the buffer section can blow the material adhered to the filter into the conical hopper, avoiding material blockage of the filter. The weighing module above can improve the accuracy of weighing and measurement, with a high degree of automation.







