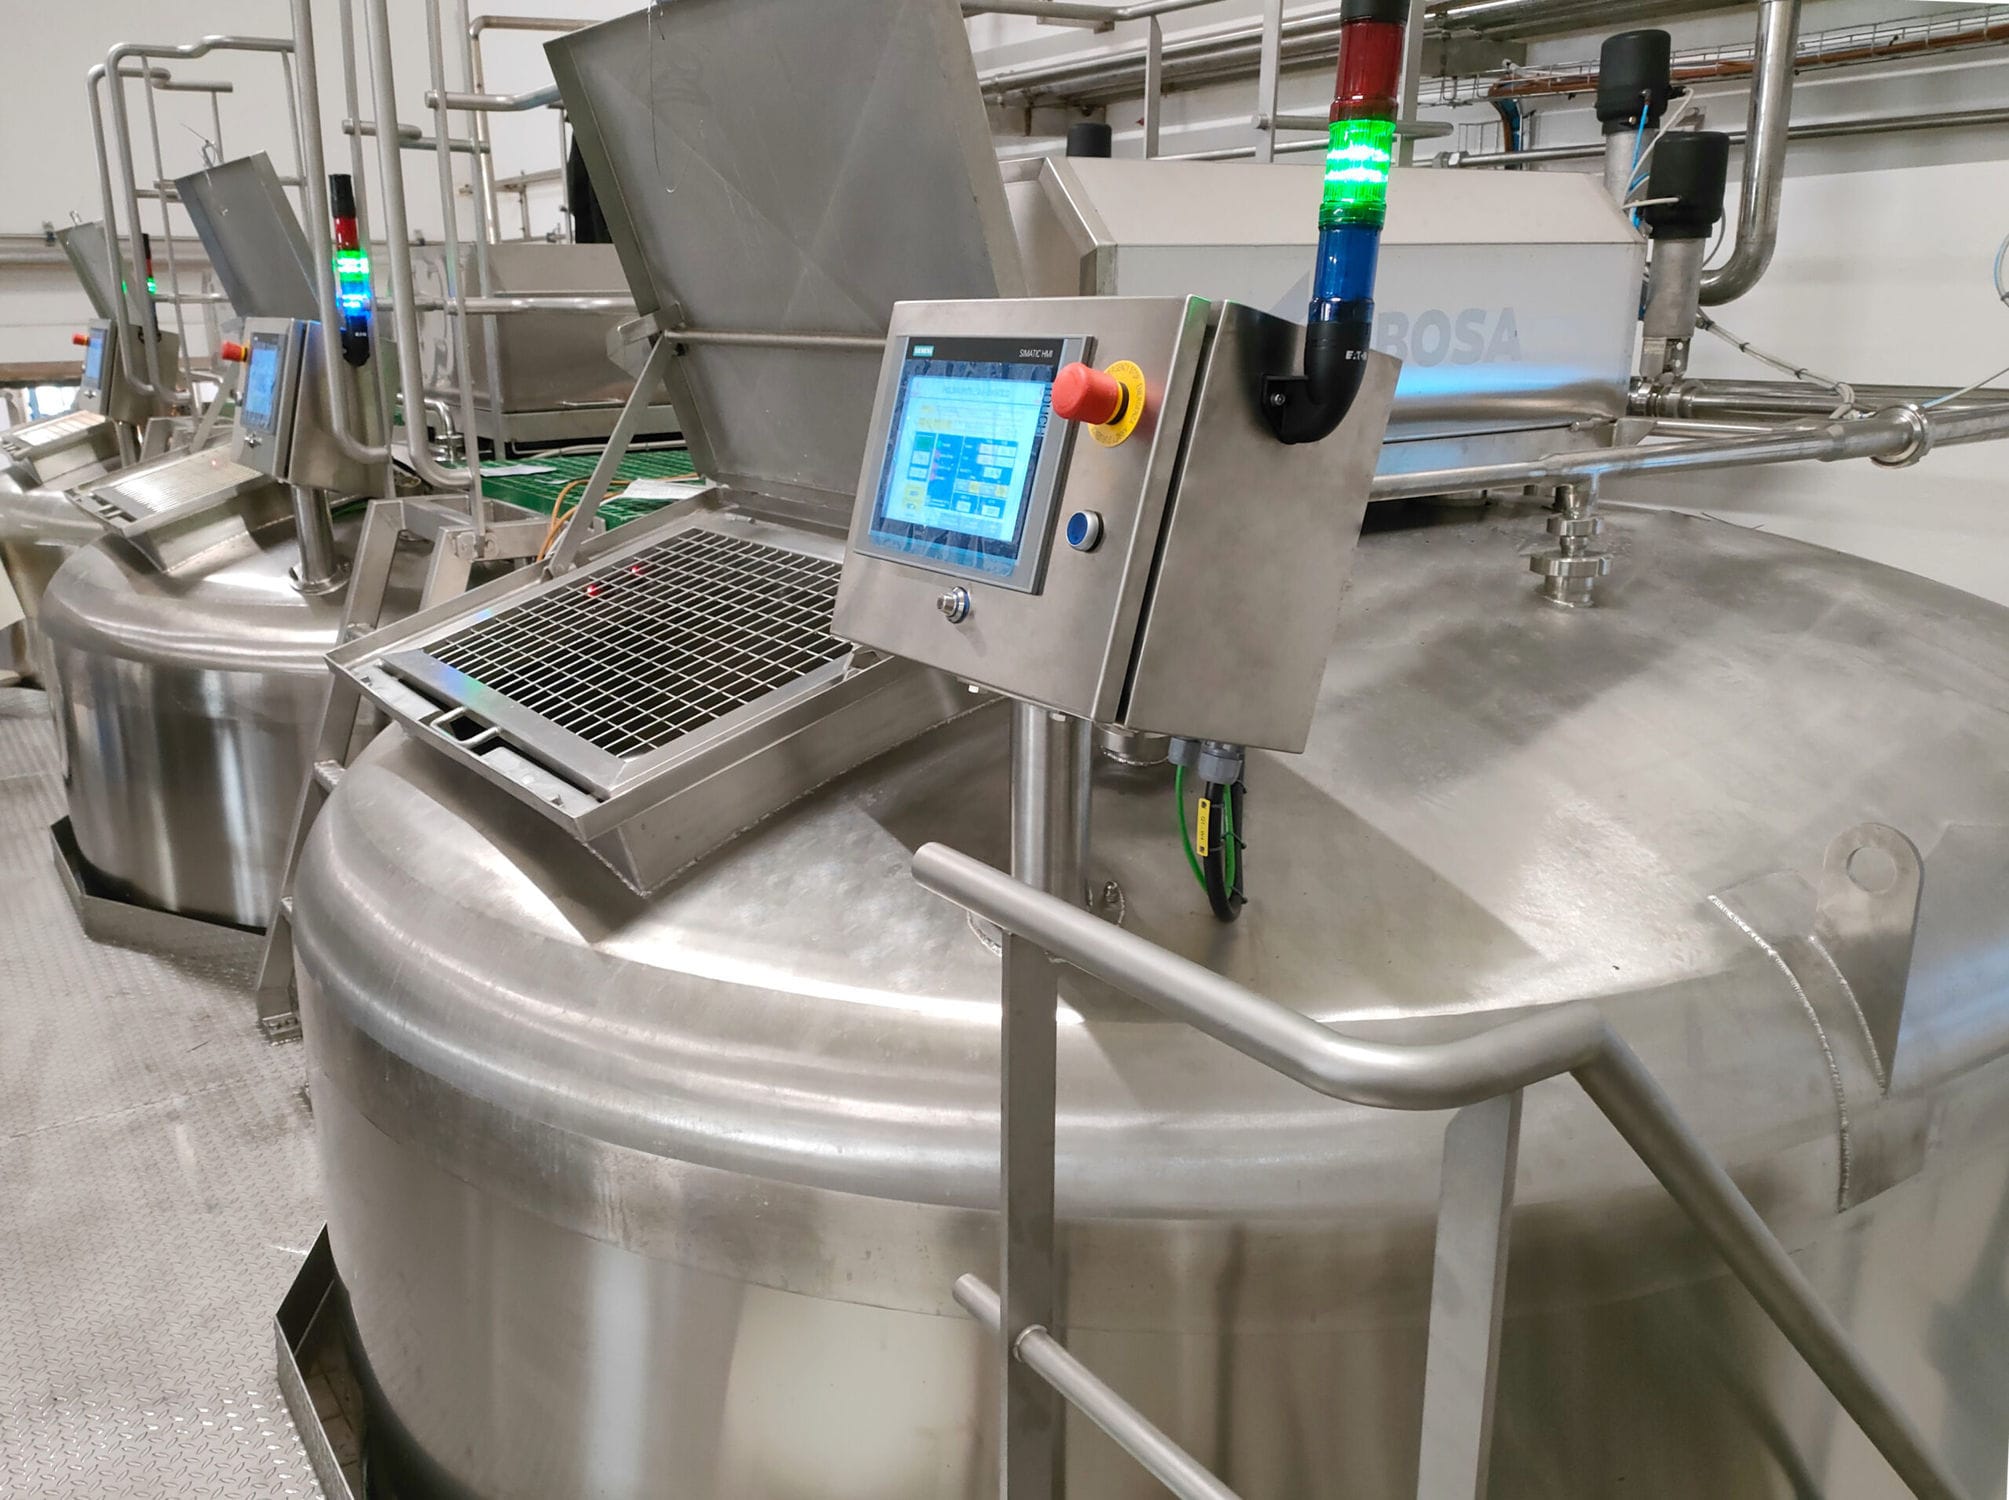
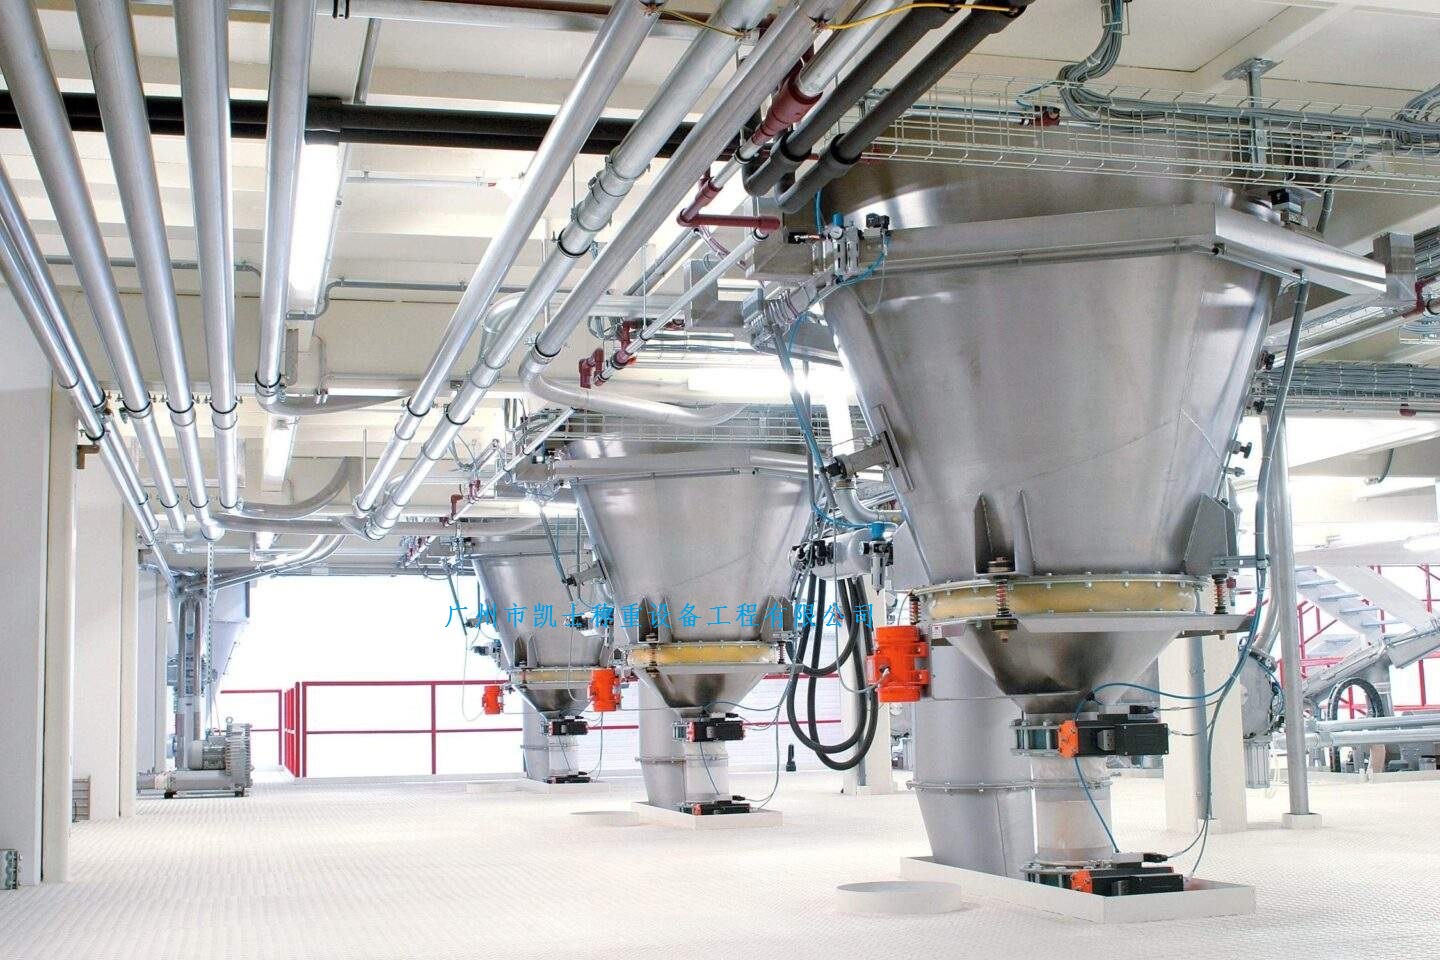
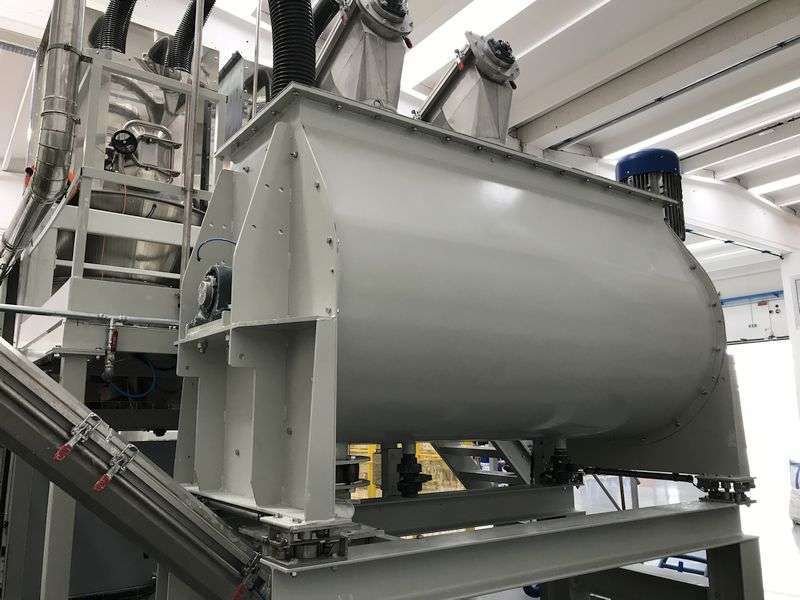
The weighing screw system is composed of a driving part, a double-layer screw stirrer, a U-shaped barrel and a weighing module. The rotation direction pushes the material from both ends to the middle, and the inner screw pushes the material from the middle to both ends. The different angles and directions of the screw belt wind the material in different flow directions, and the material is rapidly mixed through continuous convection circulation and shear mixing. Pneumatic gate valve is set up in the center of the bottom of the horizontal cylinder, and the spiral structure of the outer spiral belt with the rotation direction of the main shaft drives the material inside the cylinder wall to the central outlet. The pneumatic gate valve is designed to control the lead amount of the end feed, so as to reduce the impact of the drop on the batching accuracy and keep the actual batching value within the error range.


 020-34563445
The weighing screw system is a hopper scale equipment that integrates feeding and measuring, and can achieve continuous dynamic feeding and measuring of granular materials. Adopting the principle of constant speed and quantitative feeding, it consists of a feeding screw, a measuring screw, a weighing module, and a control system, which can monitor and adjust the material flow rate in real time. Based on continuous dynamic feeding measurement, the working principle of constant speed quantitative feeding scale is adopted to integrate feeding conveying, weighing measurement and quantitative feeding control functions into one, forming an electromechanical integrated continuous dynamic feeding measurement equipment. The weighing hopper machine consists of transmission components, double-layer spiral bar agitator, U-shaped bucket body, and weighing module. The rotating direction pushes the material from both ends to the middle, while the inner spiral bar pushes the material from the middle to both ends. The different angles and directions of the spiral belt create different flow directions for the material, and the material is rapidly mixed through continuous convection circulation and shear mixing. A discharge port with a pneumatic gate valve is set up at the center of the bottom of the horizontal cylinder. The spiral structure of the outer spiral belt is matched with the rotation direction of the main shaft to drive the material inside the cylinder wall to the central discharge port for discharge. The pneumatic gate valve adopts a termination feeding advance to control the termination feeding advance, in order to reduce the impact of the drop on the batching accuracy and keep the actual batching value within the error range.
The weighing control system transports piles of materials from the coarse feeding hopper to the hopper scale. The upper and lower hopper scales of the hopper scale interlock and close at a certain frequency to weigh 90% of the predetermined weight of the material. Then, the weighing screw machine transports the weighed material to the Electronic scale, which measures the accurate weight of the material and sends a signal to the control element. The control element receives the signal, analyzes it, and sends a control signal to the fine feeding mechanism to control the fine feeding mechanism to transport the remaining weight of the material to the hopper of the electronic scale. During the conveying process, the electronic scale dynamically weighs the weight of the material on the hopper and sends a signal to the control element. When the weight of the material on the hopper reaches the predetermined weight, the control element Send a signal to the motor that controls the push plate, The motor drives the push plate to push the material on the hopper to the mixing mechanism.
The weighing screw machine is transported from the feeding port to the connected measuring electronic scale through a screw conveyor. The weighing sensor installed on the measuring electronic scale detects the weight of the material and generates a voltage signal proportional to the weighing load, which is sent to the controller. Together with the preset speed data of the electronic scale (during measurement, the measuring electronic scale operates at a constant speed, that is, the speed signal is the design value of the measuring electronic scale), the instantaneous flow rate and cumulative weight value are calculated. The control system compares the actual flow signal with the set flow signal, and outputs a control signal to the frequency converter through PID regulation to dynamically adjust the speed of the feeding cutter, thereby achieving quantitative feeding. Due to the height difference between the discharge port of the feeding drum and the electronic scale, the material in this height difference will cause errors. If dynamic control is chosen, there will be errors regardless of how the control components send control signals to the motor that controls the feeding drum. The control component only sends a control signal when the weight of the material on the electronic weighing hopper is the same as the predetermined weight, and the feeding drum can stop feeding on time. There is still a continuous flow of material between the material surfaces on the feeding outlet hopper that needs to fall into the hopper scale, which also causes measurement errors. Therefore, reducing the distance between the feeding device outlet and the hopper scale and reducing the amount of material flow during feeding is necessary.