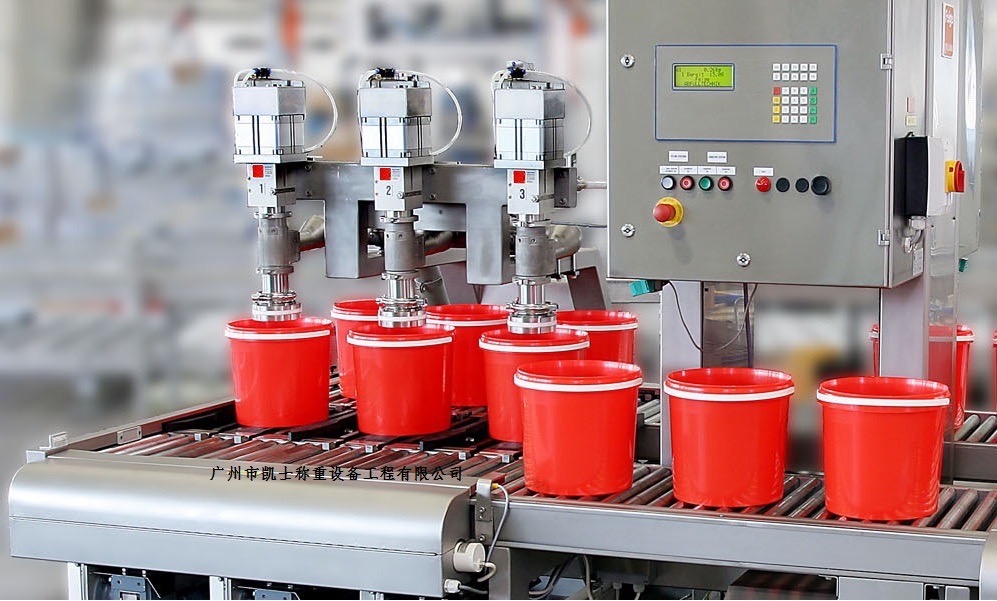
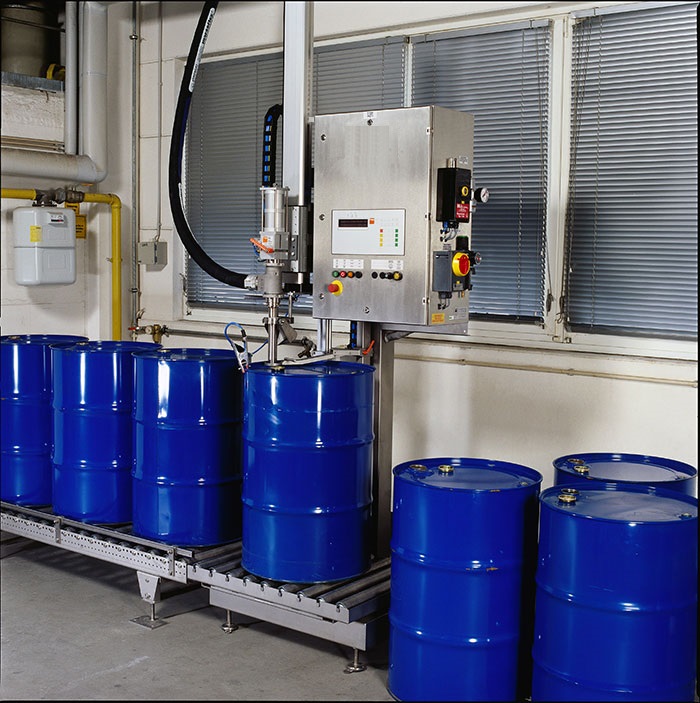
The quantitative paint filling machine collects input signals for weight through the industrial control computer and PLC, and after processing by the program, issues control commands for quantitative filling to the filling mechanism. It realizes on-site information collection and system communication through open fieldbus and industrial Ethernet. The metering filling system using mechatronics technology consists of PLC and weighing instruments for measuring and controlling the filling process of weighing, metering and filling in the production workshop.

 020-34563445
The weighing and Filling machine consists of Electronic scales, weighing instruments PLC、 It consists of components such as feeding frequency converter, material conveyor frequency converter, feeding and filling gun, limit switch, proximity switch, and industrial computer. In the filling process of the raw material quantitative filling machine, the filling process can be divided into four main production stages: quantitative setting, weighing, dropping, and conveying of four types of materials. The production equipment involved includes material warehouses, containers, conveying rotary pumps, conveyors, electronic scales, and discharge filling guns. The material is transported from the raw material yard through the pipeline to the filling gun, and the conveying Feeder quantitatively drops the material into the container according to a certain target amount. The filling and conveying system uses a rotor pump for variable frequency feeding. The filling gun at the top of the container is opened, and the material falls from the filling gun into the container on the electronic scale. The conveyed material is sent into the container through the frequency converter, and the unloading piston of the filling gun is opened to finally deliver the material into the container. The Liquid filling machine collects input signals through an industrial computer and PLC, processes them through a program, and sends control quantitative commands to the filling mechanism. It uses an open fieldbus and industrial Ethernet to achieve on-site information collection and system communication, and uses a measurement and Filling system based on mechatronics technology. PLC and weighing instruments form a measurement and control system to complete the production process of weighing, measuring, and filling. Equipped with electronic scales, pneumatic actuators, electric actuators, automatic control components, and filling devices, it achieves online weighing and filling work. Three signals are sent from the PLC, namely tare weight removal, tare weight reset, and data retention; Before each weighing, the tare weight should be removed first, and the net weight should be immediately set to zero. After the final weighing value is reached, the data should be retained. After the discharge is completed, the tare weight should be reset, and the skinning operation should be canceled. At this time, the gross weight and net weight are the same value, which can ensure the net weight of the filling for each weighing. There are 5 signals sent to the PLC, namely near zero, preset value, drop value, insufficient, excessive, and upper limit.
The automatic filling machine consists of main parts such as feeding mechanism, Weighing system, unloading mechanism, and discharging mechanism. The feeding mechanism consists of a material preparation warehouse and a rotor pump feeding device. The material preparation warehouse is used to store the filled materials, while the rotor pump feeding device transports the materials to the material preparation warehouse through the rotor pump. The weighing system consists of containers PLC、 Composed of stainless steel weighing scales, text displays, and cylinder liners. The PLC is connected to the electronic weighing scale to detect whether the weight of the material in the container meets the actual required value. By filling the piston valve, the material in the container meets the standard value requirements. The unloading mechanism consists of an unloading door and a filling cylinder, used to complete the unloading of materials from the container. The feeding mechanism consists of a feeding bin and a filling gun, used to complete the filling of materials. To achieve the purpose of convenient weighing mentioned above, two fixed bases are used. The top of the two fixed bases is fixedly installed with a material bucket weighing scale, and the top of the filling weighing scale is fixedly installed with a pressure rod. The top of the pressure rod is fixedly installed with a placement plate. When the rotor pump places the material into the preparation bin by the feeding device, the material enters the filling bin through the feeding plate under the action of the pump. The filling piston valve of the filling bin is opened by 95%, and two types of filling are carried out for the material: coarse feeding and fine feeding (when the bin door is opened, coarse feeding enters, 5% is opened, and coarse feeding stops, and fine feeding is carried out). The material enters the container through the filling bin, and when the container reaches the given point, it enters the When the weight of the coarse material is added, the warehouse door is half closed and enters the fine feeding state. When the weight of the container reaches the given target weight, completely close the filling piston valve and stop fine feeding. Complete the filling process.
The weighing and filling machine includes a variable frequency motor, gear pump, suction tube, feeding tube, fast and slow dual position filling valve, dual position stroke cylinder, electromagnetic reversing valve, electric control box, double-layer weighing scale, filling bucket and calibration bucket device. The suction tube is fixedly installed on the suction port of the gear pump, and one end of the feeding tube is connected to the fast and slow dual position filling valve, and the other end is connected to the discharge port of the gear pump. The gear pump is driven by a variable frequency motor, and the dual position stroke cylinder is installed on the fast and slow dual position filling valve. The dual position stroke cylinder is connected to the compressed air source through two electromagnetic reversing valves. The filling weighing scale is located below the fast and slow dual position filling valve, and the filling bucket is placed on the material tank weighing scale. The electromagnetic reversing valve, weighing scale, and variable frequency motor are all connected to the electrical control box, and the bucket calibration device is symmetrically distributed on both sides of the filling bucket; The electromagnetic directional valve is a two position five way directional valve; The fast slow dual position filling valve includes a valve body, a push rod, a filling nozzle, a valve core, and a feeding port. The filling nozzle is screwed onto the valve body, and the valve core is fixed at the lower end of the push rod. The push rod is placed inside the valve body and the filling nozzle, and is fixedly connected to the lower piston in the dual stroke cylinder. The upper piston is located above the lower piston, and both the upper and lower pistons can be installed in the inner hole of the cylinder block in a sliding manner. When the metering filling machine is in automatic operation, according to production requirements, the target amount of material is input through the keyboard in the PLC, and the fast dispensing target value and standard setting value of the material are calculated by the PLC. When the fast filling target value of the material is less than the standard setting value, the PLC sends a high-speed command to make the conveying material work in a high-frequency state, and the material quickly falls into the container to improve feeding efficiency. At the same time, the net weight of the material is displayed in real time on the PLC. When the material reaches the set fast filling target value, the frequency converter switches to a smaller conveying frequency and feeds slowly; When the weighing value is less than the standard set value of the material (if the difference is outside the allowable range), the PLC will automatically start jog correction, and the material will continue to be filled to ensure filling accuracy; If the difference is within the allowable range, the PLC will output a stop signal, and the conveying and feeding will stop running, ending the conveying and feeding process. Complete the filling cycle of a batch.
The filling bucket input by the bucket conveying mechanism of the automatic filling machine is quickly pushed into the waterproof weighing scale by the bucket calibration device, and the weight of the bucket body is weighed. This signal is input into the electric control box, which then sends corresponding electrical signals to the variable frequency motor and two electromagnetic reversing valves, making the variable frequency motor in working state, so that the upper and lower pistons in the dual stroke cylinder are in the pushing position, and the valve core at the lower end of the push rod is in the downward limit position. At this time, the filling section between the filling nozzle and the valve core is the largest. When the filling is close to the predetermined filling weight, the explosion-proof weighing scale inputs relevant information to the electric control box and controls the dual stroke cylinder, so that the upper piston is in the lower position and does not move, and the lower piston moves upward, thereby reducing the filling section between the filling nozzle and the valve core and achieving slow filling. When the filling weight reaches the predetermined amount, the weighing scale sends an electrical signal to the electrical control box, Reset both the upper and lower pistons in the dual stroke cylinder to their upper positions. At this point, the filling section between the filling nozzle and the valve core is completely closed. Then, the filled barrel body is output by the barrel conveying mechanism and enters the capping machine.