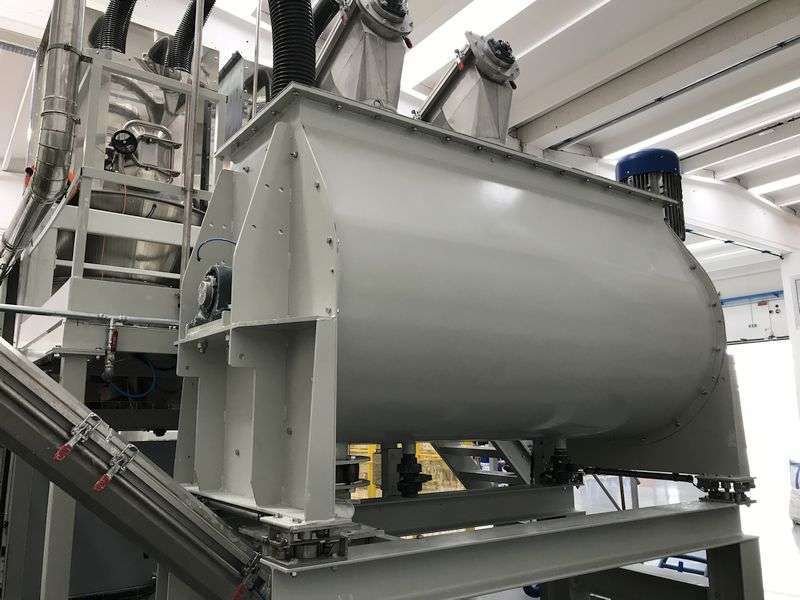
The operation commands and setting parameters issued by the assembly weighbridge on the upper computer can be sent in real time to the PLC. The PLC receives the commands sent by the upper computer and controls the start, stop, and speed of the vibration motor through the frequency converter. The operating status of the frequency converter is written in real time to the memory data area for the industrial control computer to read. The various states of the weighbridge are prepared in the form of status words and are ready for the industrial control computer to read in real time.

 020-34563445
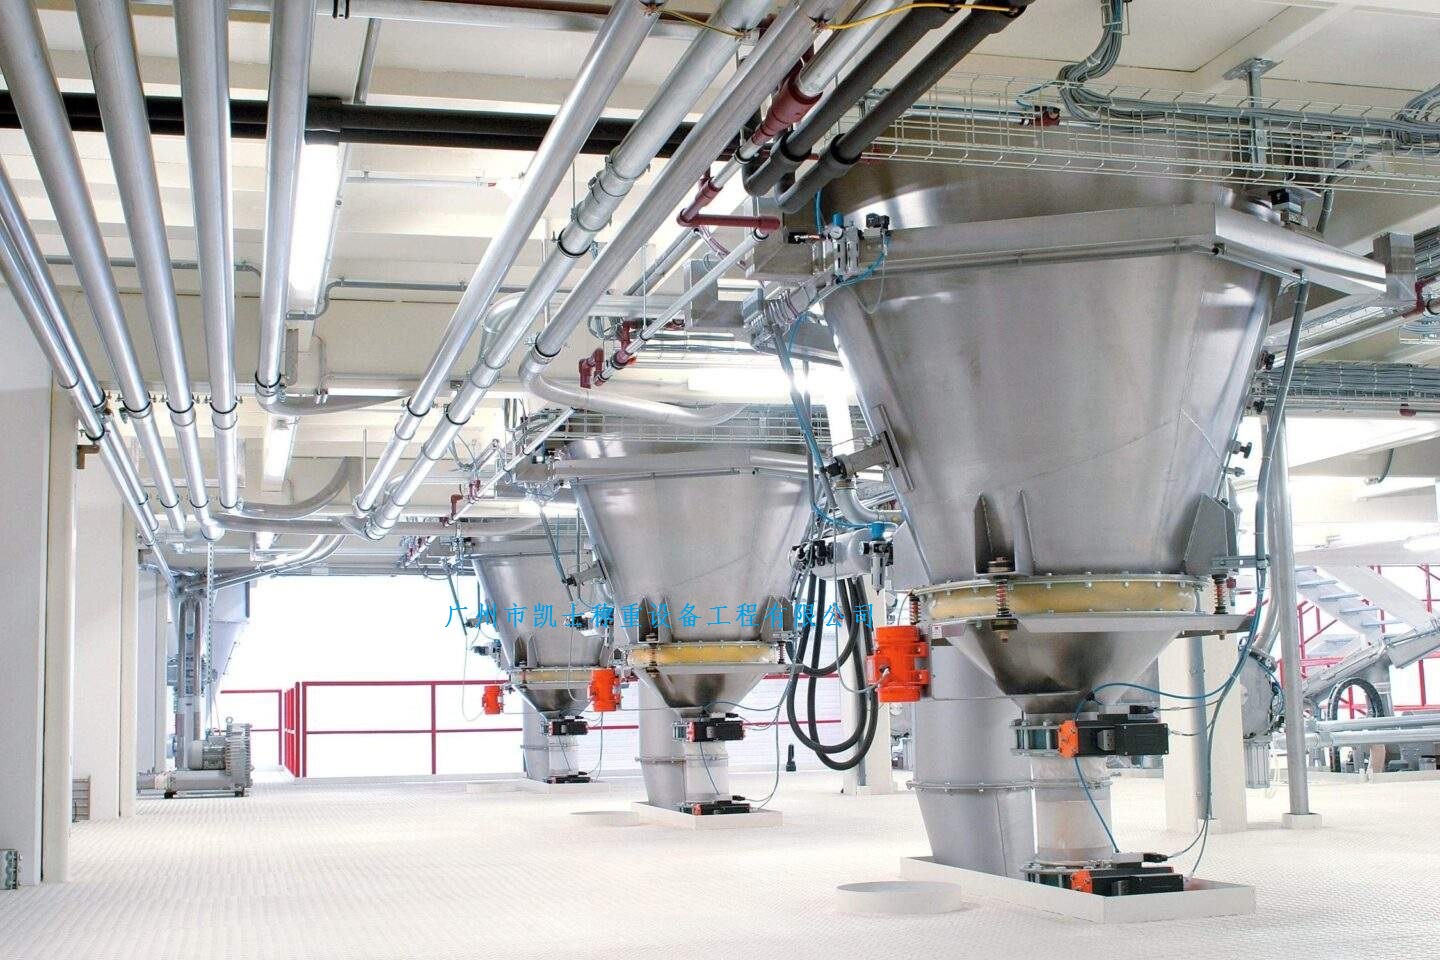
Assembly of the weighing platform involves using high-speed gas flows of nitrogen or air, through nozzles, to suspend the powder in the pipeline. The suspended powder, propelled by the high-speed gas flow, is transported along the sealed pipeline to the final user. The electronic weighing platform under the silo measures and controls the process and activates the Roots blower. The control of the Roots blower can be accomplished by a complete controller; start the bag filter, which blows compressed air to the bags in a pulse form according to the set program to remove dust on the bag surface; open the shaft seal air valve XV-4101 of the rotary feeding valve (blowing valve). After completing these steps, check if the wind pressure meets the requirements. If it does, the feeding process can start, and activate the rotary feeding valve 4X01. The powder enters the feeding silo through 4X01 and then enters the nozzle, where the powder is suspended in the pipeline under the high-speed gas flow and is transported forward along the sealed pipeline into the 1# or 2# powder receiving silo. Whether to enter the 1# or 2# receiving silo can be achieved by the reversing valve XV-3101, which is equipped with a valve position switch. Each receiving silo is equipped with upper and lower capacitive level switches to determine whether the silo is allowed to be filled.
The Electronic scale control system is based on the Siemens PLC as the control core. It is equipped with a high-performance electronic scale that communicates with the PLC, used for displaying process status and performing action control, and also sending operation instructions to the system. According to the on-site conditions and process requirements, the on-site environment is a dust explosion-proof environment. On-site instruments use explosion-proof instruments. The signals from the on-site instruments are sent to the PLC for status indication and interlock control. The PLC performs interlock control based on the stored interlock control program, starting or closing the on-off of relevant valves, sending on-off signals to start or stop the bag dust collector, rotary feeding valve (blower) 4X01 and Roots blower, etc. The on-off signals are fed back to the PLC, and introduced into the interlock control loop to ensure that all equipment is in the correct state. Finally, the powder is transported through compressed air along the closed pipeline to the boundary external silo.